Professional industrial water treatment equipment manufacturer in China, specializing in RO systems, reverse osmosis equipment, water purification systems, wastewater treatment and customized water treatment solutions for global industries.
Professional industrial water treatment equipment manufacturer in China, specializing in RO systems, reverse osmosis equipment, water purification systems, wastewater treatment and customized water treatment solutions for global industries.


What water treatment equipment is used for boilers? How to choose between water softening equipment
What water treatment equipment is used for boilers
The long-term stable operation of a boiler imposes very strict requirements on the quality of the feed water. If the water contains excessive calcium and magnesium ions, sediment, suspended solids, and other impurities, scale can easily form inside the boiler. This not only reduces thermal efficiency but also increases energy consumption, and may even lead to boiler corrosion, pipeline blockage, and equipment failure.
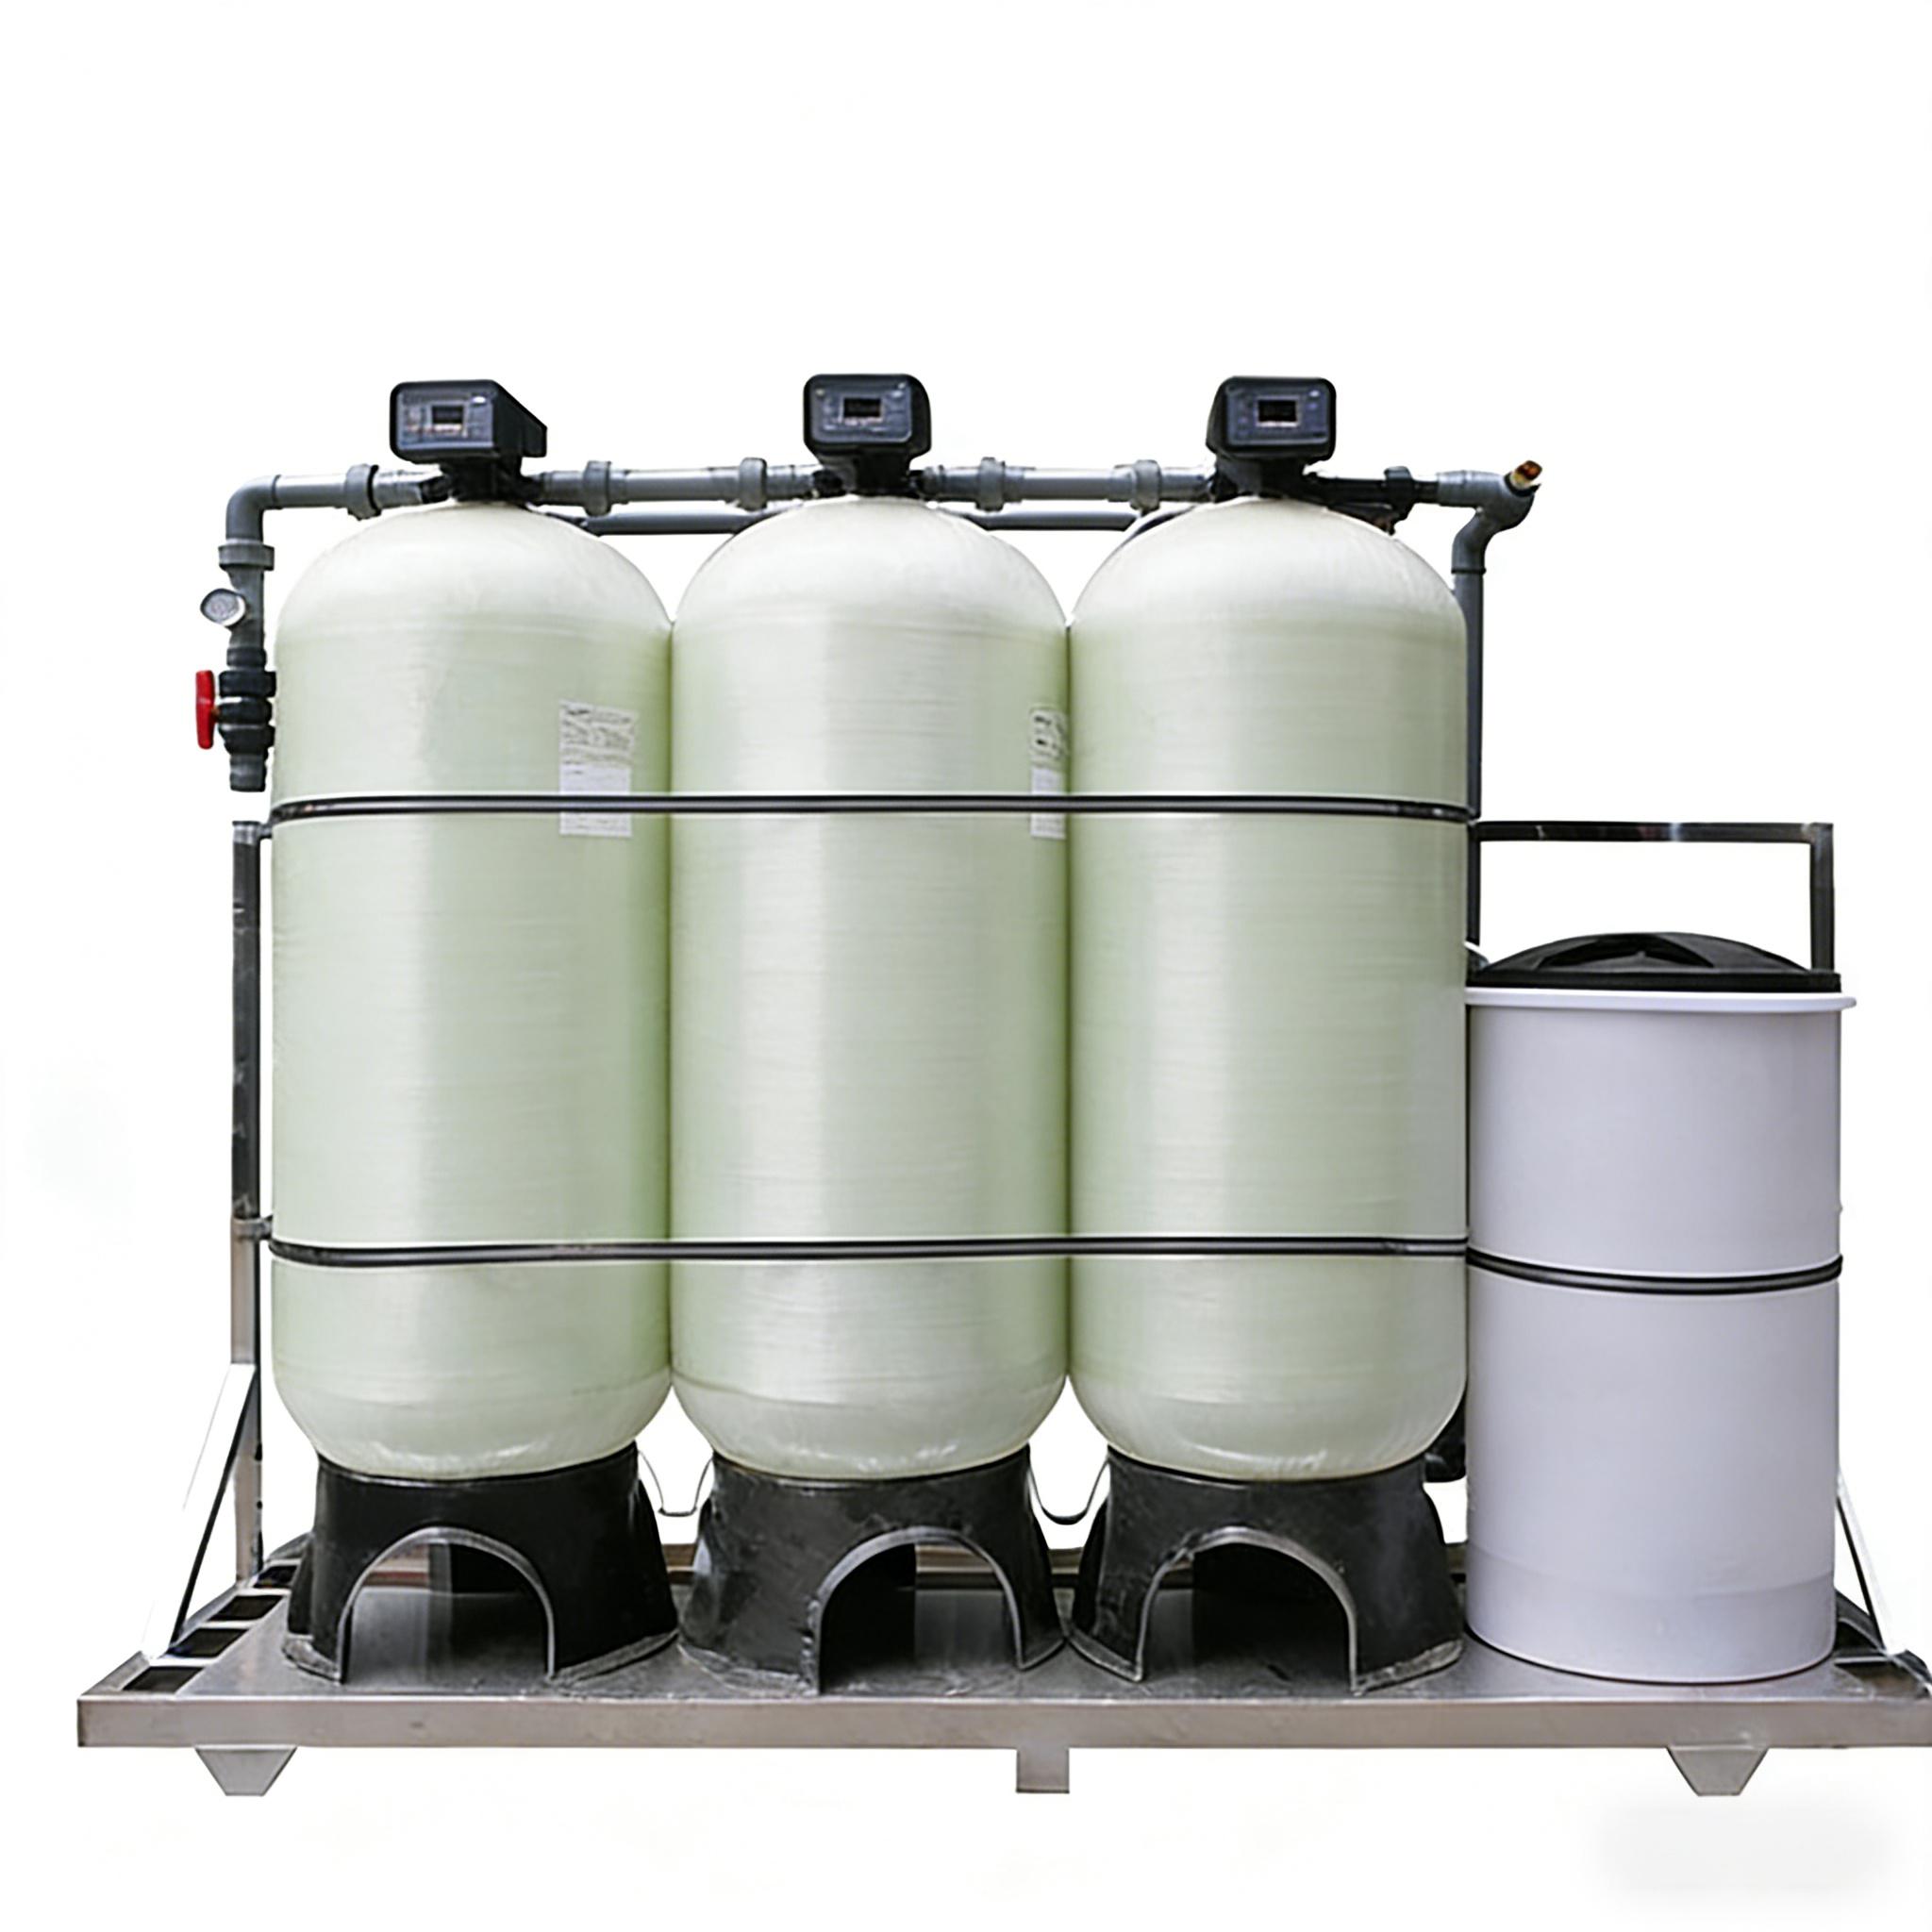
Therefore, most industrial boilers are equipped with professionalboiler water treatment equipment. Currently, the most widely used types mainly includewater softening equipmentandreverse osmosis (RO) pure water equipment. The specific choice of solution depends on the type of boiler, its pressure level, and the actual water quality requirements.
Why do boilers need water treatment equipment?
In production and daily life, untreated raw water usually contains high concentrations of calcium and magnesium ions (hardness), iron and manganese, suspended solids, and organic matter. When these impurities enter the boiler, they gradually form scale and deposits, which can lead to the following problems:
Causing boiler scaling and shortening the service life of the equipment;
Triggering pipeline blockage and corrosion;
Increasing costs for shutdown cleaning and maintenance;
In severe cases, potentially affecting the safe operation of the boiler.
These problems can all occur during long-term use. Therefore, to ensure stable operation, boiler manufacturers typically require a certain quality of the water source. As a result, proper treatment of the feed water before commissioning is an important measure to ensure stable and efficient equipment operation.
Steam boilers generally use reverse osmosis equipment
For boilers that need to generate steam, it is usually recommended to usesingle-stage reverse osmosis (RO) water treatment equipmentas the main purification system.
Reverse osmosis equipment can effectively remove:
Calcium and magnesium ions (reducing hardness)
Soluble salts
Heavy metals
Bacteria and viruses
Colloids and organic matter
After treatment by reverse osmosis, the desalination rate can reach over 95% to 99%, significantly reducing the risk of boiler scaling. It is suitable for:
Steam boilers
Food processing boilers
Pharmaceutical industry boilers
Chemical boilers
Textile and printing boilers
Biological fermentation boilers
For medium and high-pressure steam boilers, some projects may also usetwo-stage reverse osmosis or RO+EDI ultrapure water systemsto further improve water quality. Of course, this is quite rare, and we will not go into detail here.
Hot water boilers typically use water softening equipment
If the boiler is mainly used for heating, bathing, domestic hot water, or general industrial hot water circulation, it is usually sufficient to useresin water softening equipmentto meet the requirements.
Water softening equipment uses ion exchange resin to remove calcium and magnesium ions from the water, effectively reducing water hardness and minimizing scale formation. It offers the following advantages:
Lower equipment investment costs;
Automatic regeneration, convenient operation and maintenance;
Stable effluent quality, effectively preventing scaling;
Highly suitable for medium and low-pressure hot water boilers and heating systems.
Common applications include:
Hotel hot water boilers
School heating systems
Hospital hot water systems
Residential district central heating
Factory circulating hot water systems
How to choose the right boiler water treatment equipment?
When selecting a boiler water treatment solution, it is recommended to consider the following aspects comprehensively:
Boiler type: Steam boiler or hot water boiler;
Boiler pressure level: Low pressure, medium pressure, or high pressure;
Raw water quality: Municipal tap water, groundwater, well water, or surface water;
Hardness and TDS content: Whether desalination treatment is needed;
Boiler steam output or hot water flow rate: To determine the equipment processing capacity;
Industry standards: Industries such as food, pharmaceuticals, and electronics have higher water quality requirements.
Professional water treatment manufacturers typically design more reasonable and economical treatment solutions for customers based on raw water test reports.
Shandong Yufeng Boiler Water Treatment Solutions
Shandong Yufeng Water Treatment Equipment Co., Ltd. has over ten years of industry experience specializing in the manufacturing of industrial water treatment equipment. It can provide customized solutions based on different boiler operating conditions, including:
Boiler water softening equipment
Industrial reverse osmosis pure water equipment
Two-stage reverse osmosis systems
Ultrapure water (EDI) systems
Boiler pretreatment systems
Integrated boiler make-up water treatment systems
Whether for small heating boilers or large industrial steam boilers, we can provide efficient, stable, and energy-saving water treatment equipment based on the customer's raw water quality, water consumption, and industry requirements. This helps enterprises reduce operating costs and extend the service life of the boiler. Interested friends are welcome to discuss with us.

Address: No. 315, Jiefang Road, Lanshan District, Linyi City, Shandong Province, China

+8618553987893
yufengscl@outlook.com
Shandong Yufeng Water Treatment Equipment Co., Ltd

