Professional industrial water treatment equipment manufacturer in China, specializing in RO systems, reverse osmosis equipment, water purification systems, wastewater treatment and customized water treatment solutions for global industries.
Professional industrial water treatment equipment manufacturer in China, specializing in RO systems, reverse osmosis equipment, water purification systems, wastewater treatment and customized water treatment solutions for global industries.


Industrial Hard Water Treatment Solution for High Calcium and Magnesium Levels
Comprehensive Water Softening and Reverse Osmosis Systems for Scaling Prevention, Equipment Protecti
When hardness levels are too high, these minerals continuously precipitate and form scale such as calcium carbonate and silicate deposits. Over time, these scales accumulate on the inner walls of pipelines, boilers, heat exchangers, cooling towers, and industrial equipment.
This leads to serious operational problems, including:
Pipeline clogging
Reduced heat exchange efficiency
Equipment corrosion and aging
Increased energy consumption
Unstable product quality
Higher maintenance costs and production downtime risks
To solve these issues, a properly designed industrial water treatment system is essential.
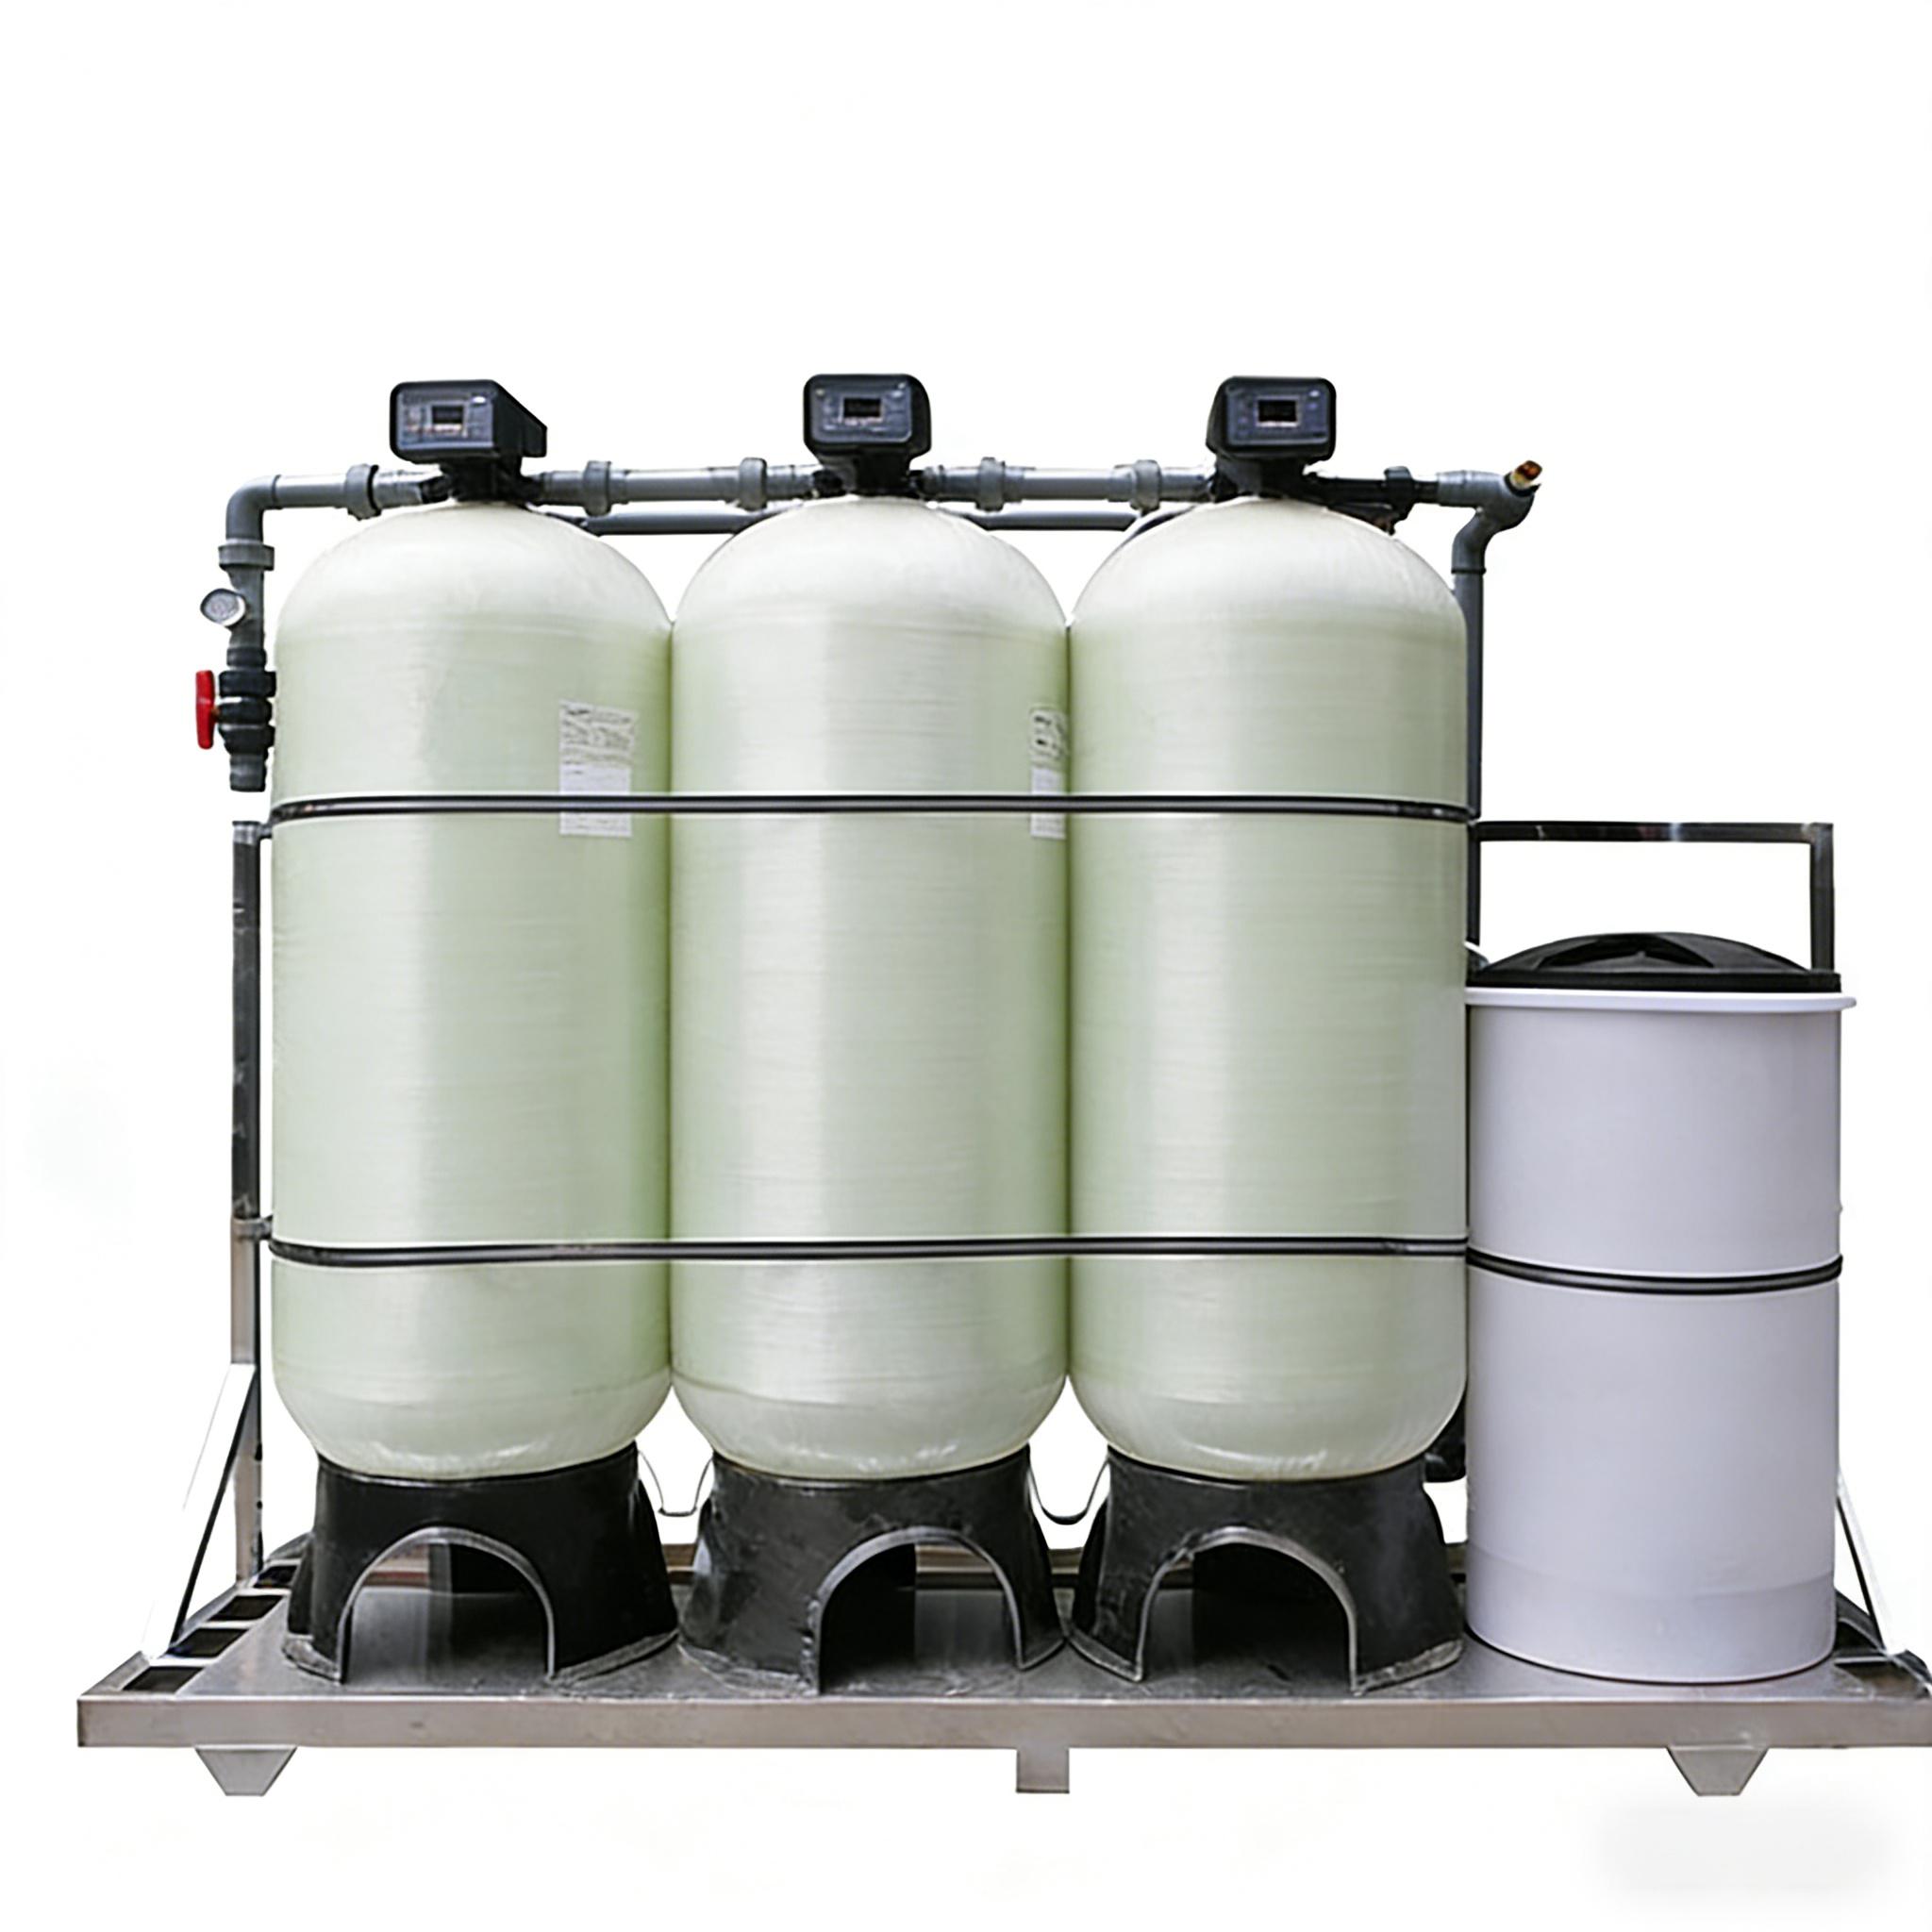
Solution 1: Water Softening System (Ion Exchange Resin)
The first method is the use of an ion exchange water softener system.
This system works by using resin to absorb calcium and magnesium ions from the water. During regeneration, softening salt (sodium chloride) is used as a consumable to restore resin performance.
Advantages:
Low operating cost
Simple system structure
Effective for reducing scale-forming ions
Limitations:
Cannot fully remove all dissolved minerals
Small amount of ions may still remain in treated water
Not suitable for very high hardness or high-purity requirements
Solution 2: Reverse Osmosis (RO) Water Treatment System
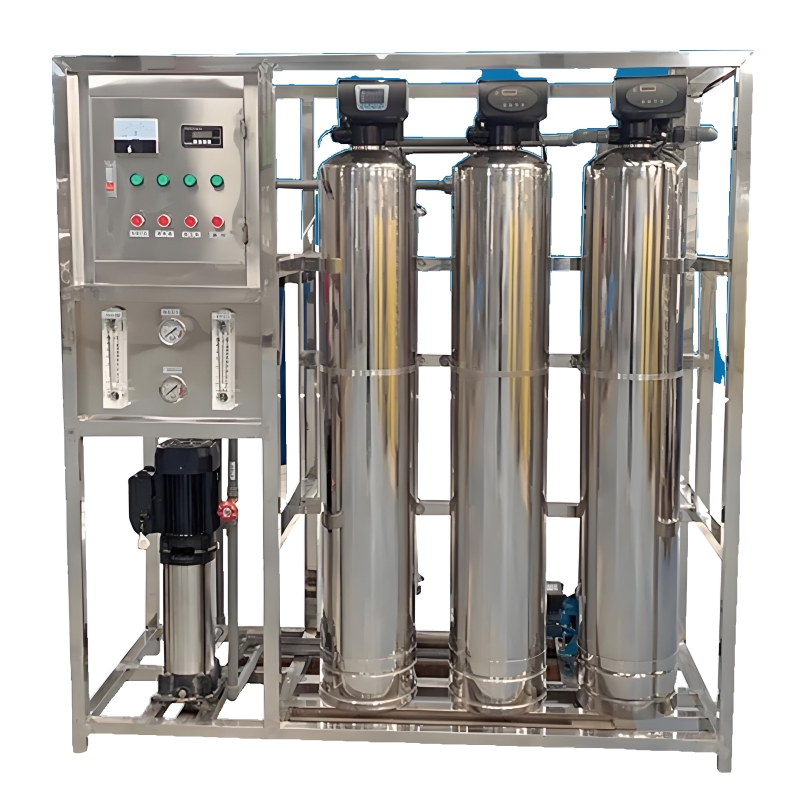
The second and more advanced solution is a Reverse Osmosis (RO) system.
RO technology uses a semi-permeable membrane to remove up to 99% of dissolved salts, including calcium, magnesium, heavy metals, and other impurities.
There are two common configurations:
RO system with antiscalant dosing (scale inhibitor)
RO system combined with pre-treatment softening system
Advantages:
Removes up to 99% of calcium and magnesium ions
Produces high-quality purified water
Suitable for demanding industrial applications
Limitations:
Higher initial investment compared to softening systems
Requires more complete system configuration and maintenance
Customized Water Treatment Design
In real industrial applications, water treatment systems are not one-size-fits-all.
Professional water treatment manufacturers typically design customized solutions based on:
Raw water quality analysis
Hardness level (calcium & magnesium concentration)
End-use water requirements
Operating cost expectations
Equipment stability and lifespan requirements
This ensures a long-term, stable, and cost-effective water treatment solution tailored to each customer’s needs.
FAQ
Q1: Can a water softener handle high-hardness well water?
Not always. Water softeners are effective for removing calcium and magnesium ions that cause scaling, but they are mainly suitable for standard water sources. A full water quality test is required before selecting a system to ensure proper design.
Q2: What applications are suitable for water softening systems?
Water softening systems are widely used in industrial circulation water systems, boiler feed water, and other non-drinking water applications. For drinking water or high-purity requirements, more advanced systems such as RO are recommended.
Q3: What is the final water quality standard?
There is no fixed universal standard. The final water quality depends on:
Raw water quality test results
System configuration and treatment process
Both factors directly determine the final output water quality.

Address: No. 315, Jiefang Road, Lanshan District, Linyi City, Shandong Province, China

+8618553987893
yufengscl@outlook.com
Shandong Yufeng Water Treatment Equipment Co., Ltd

