Professional industrial water treatment equipment manufacturer in China, specializing in RO systems, reverse osmosis equipment, water purification systems, wastewater treatment and customized water treatment solutions for global industries.
Professional industrial water treatment equipment manufacturer in China, specializing in RO systems, reverse osmosis equipment, water purification systems, wastewater treatment and customized water treatment solutions for global industries.


Industrial Reverse Osmosis Water Purification System for Superior Filtration
Industrial Reverse Osmosis Water Purification System for Superior Filtration
Product Description
Overview
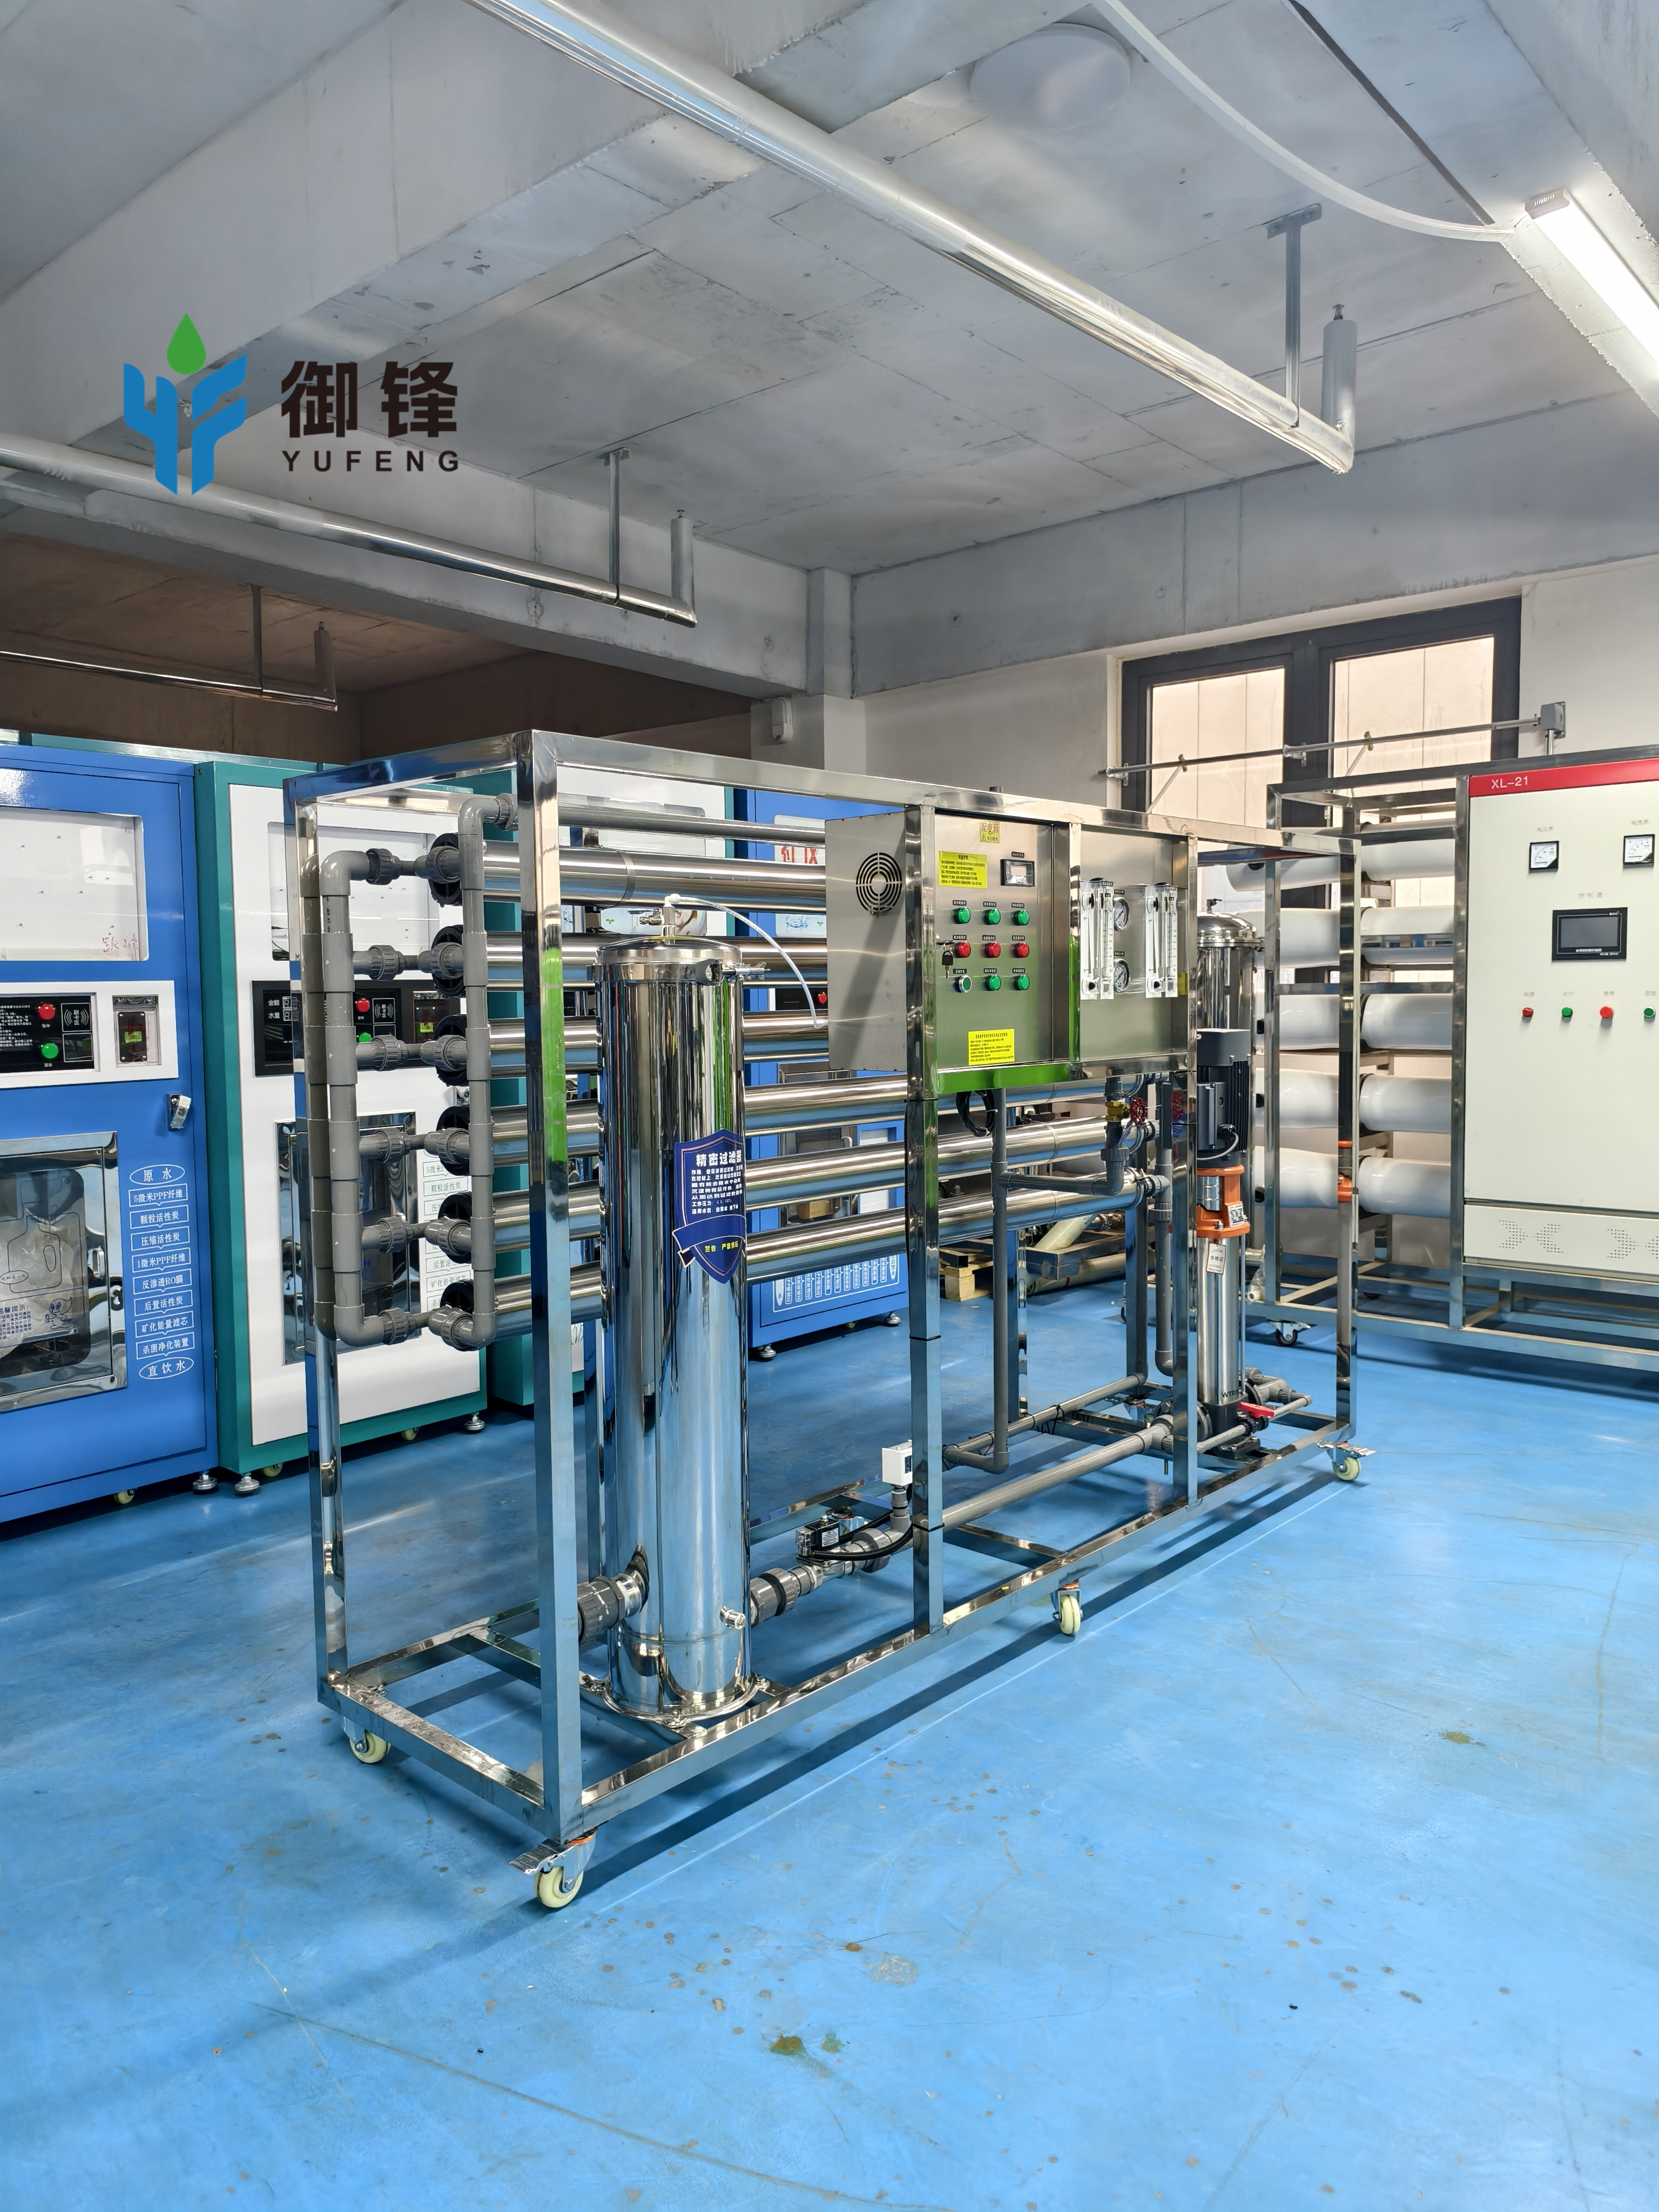
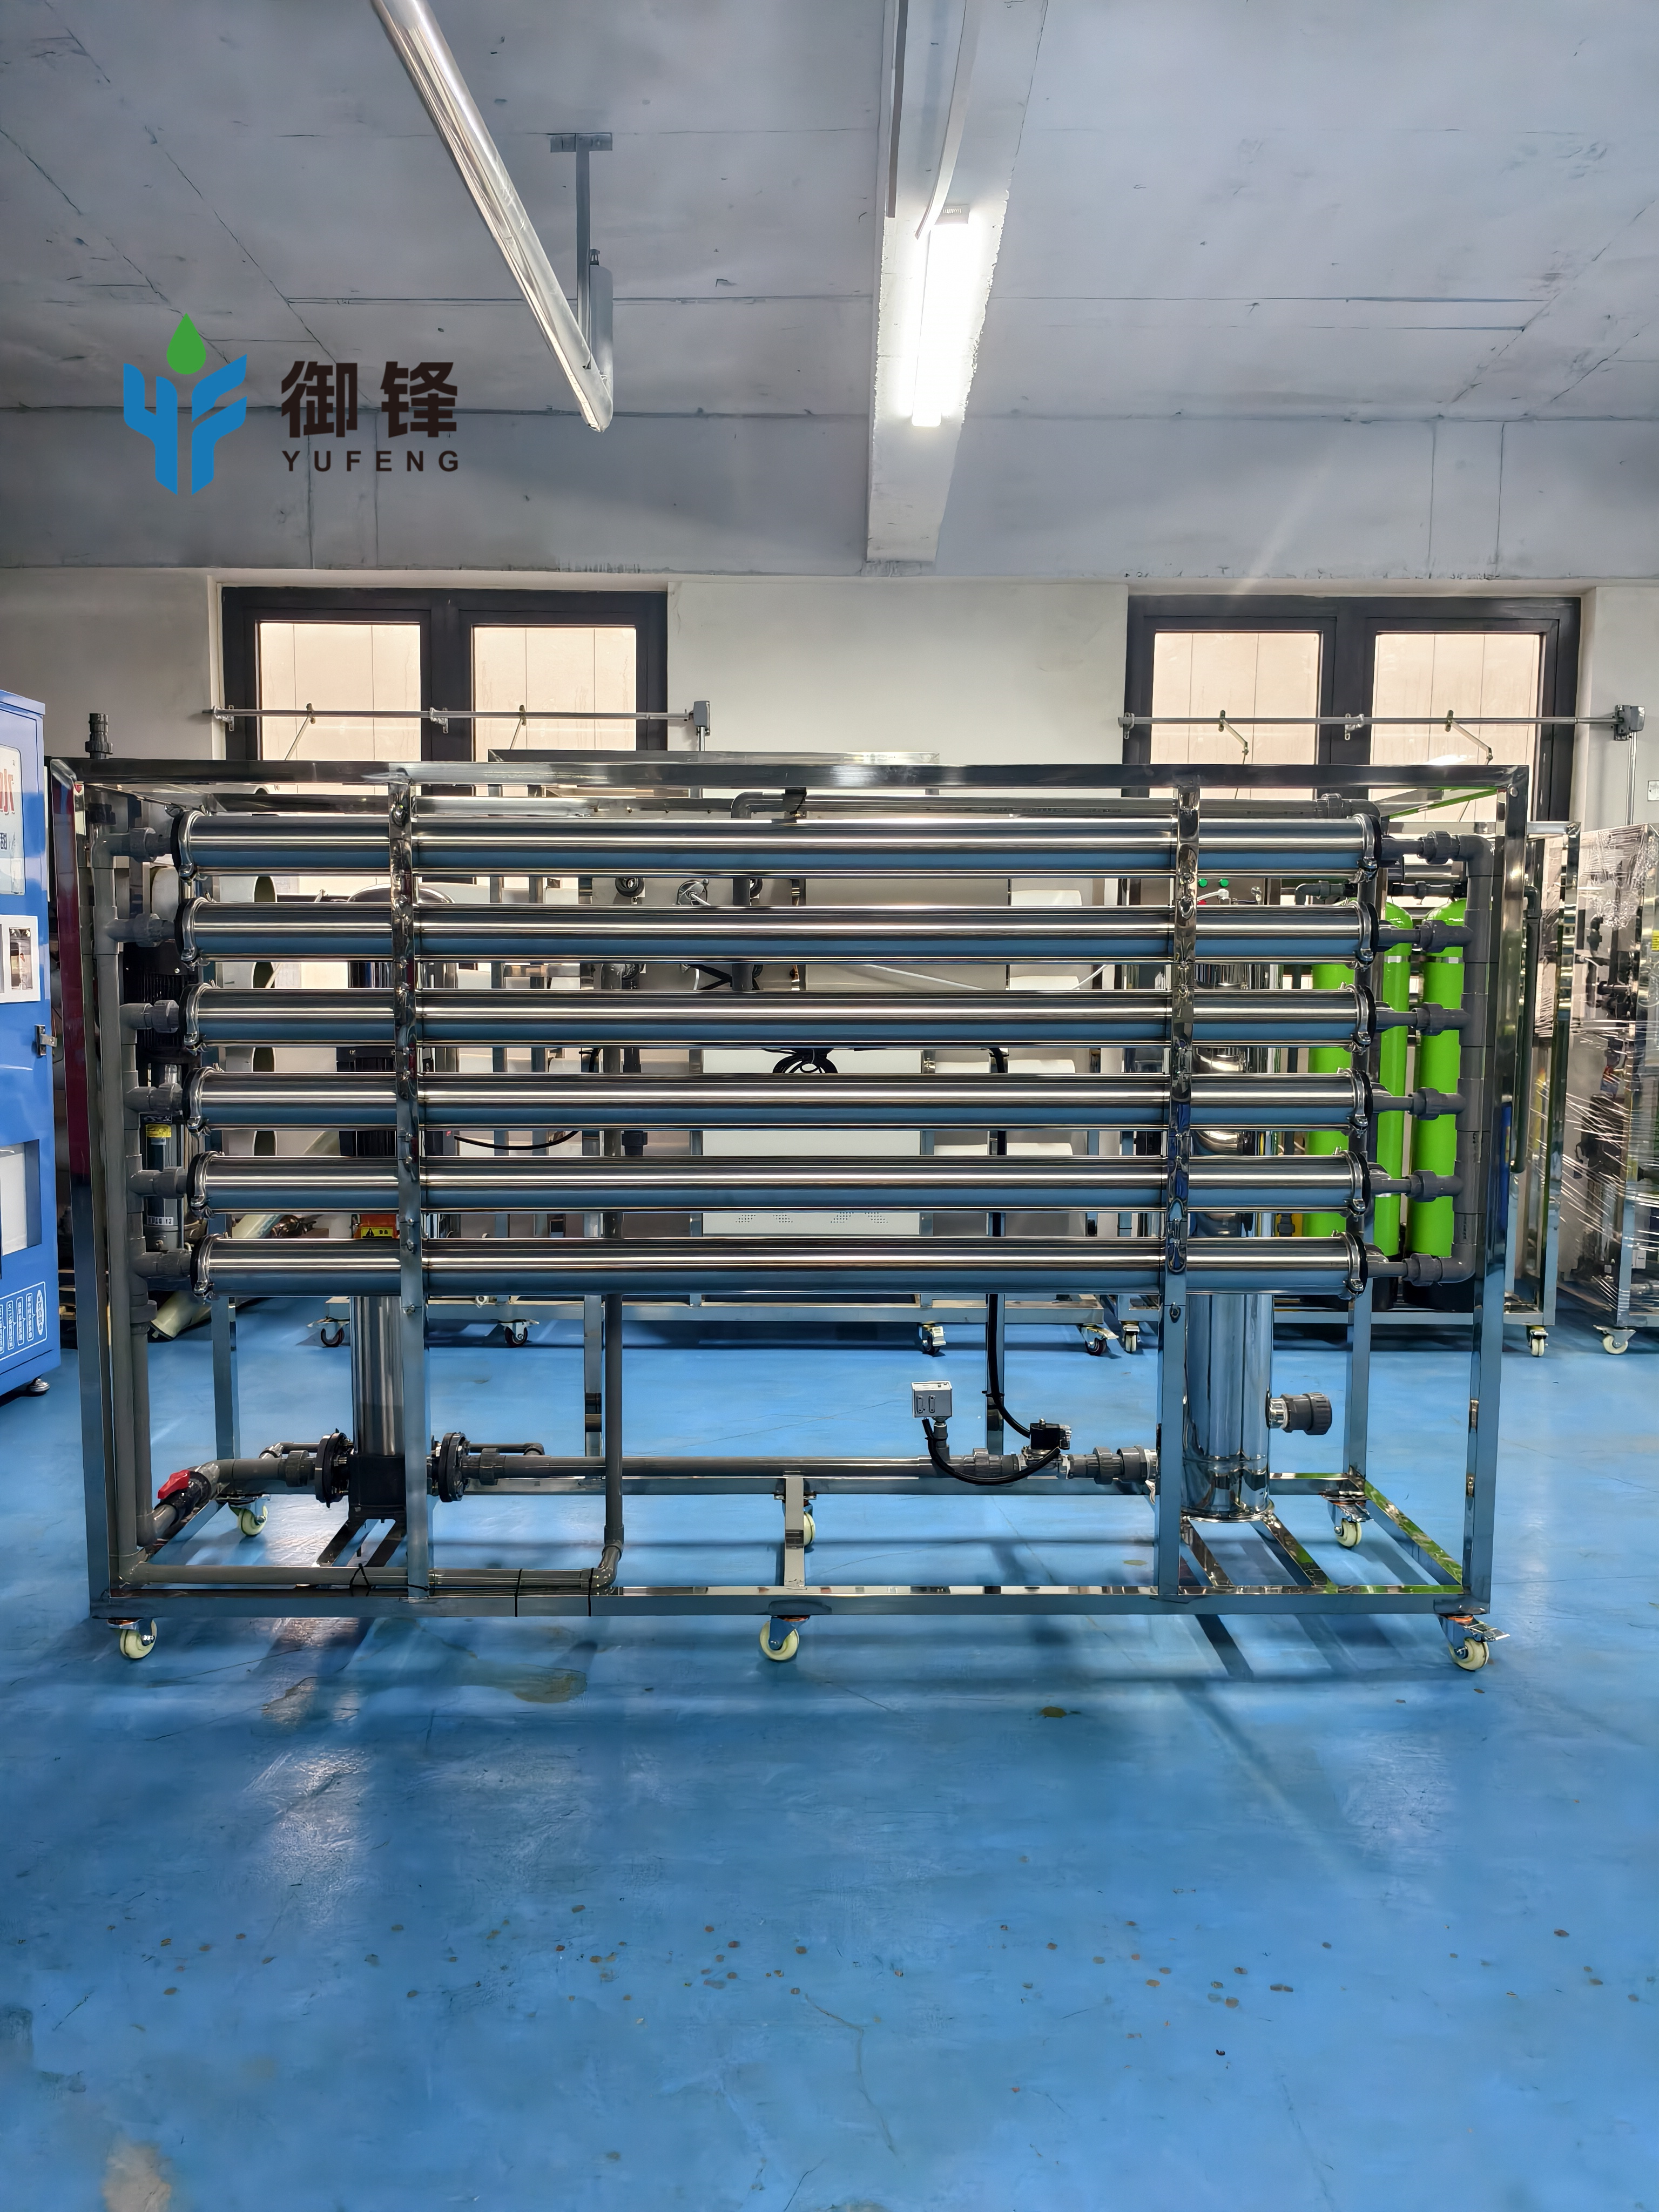
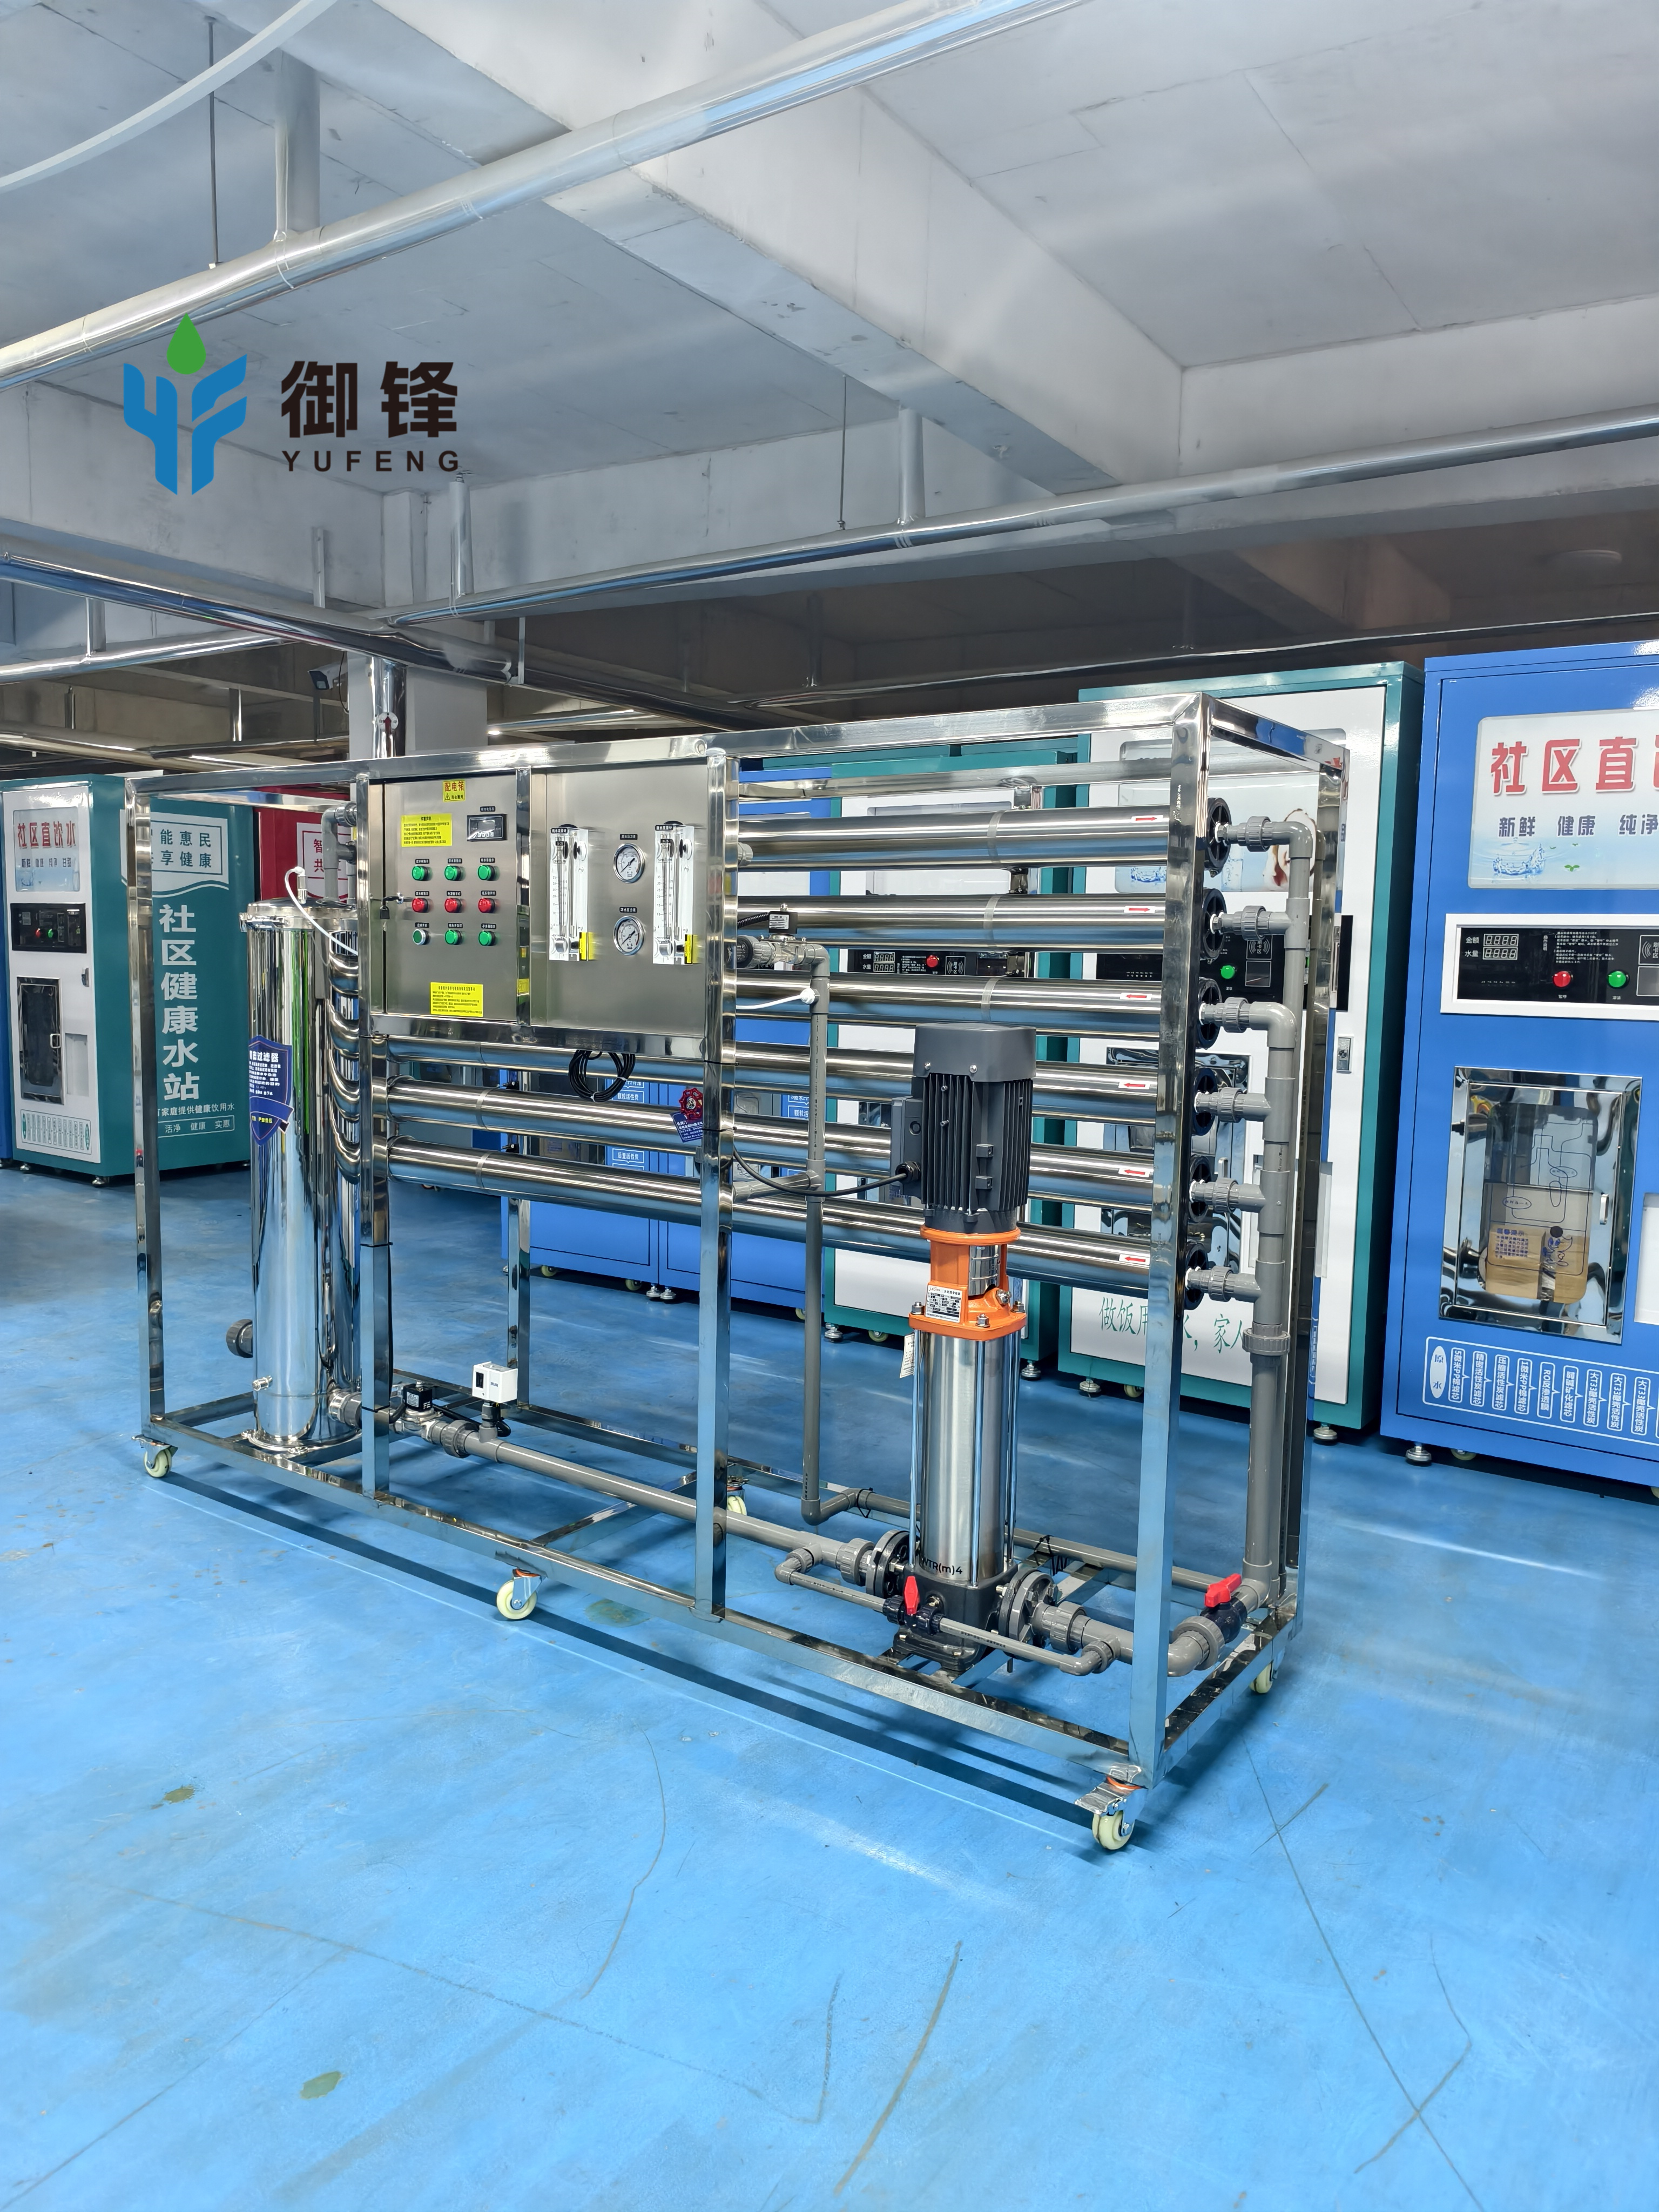
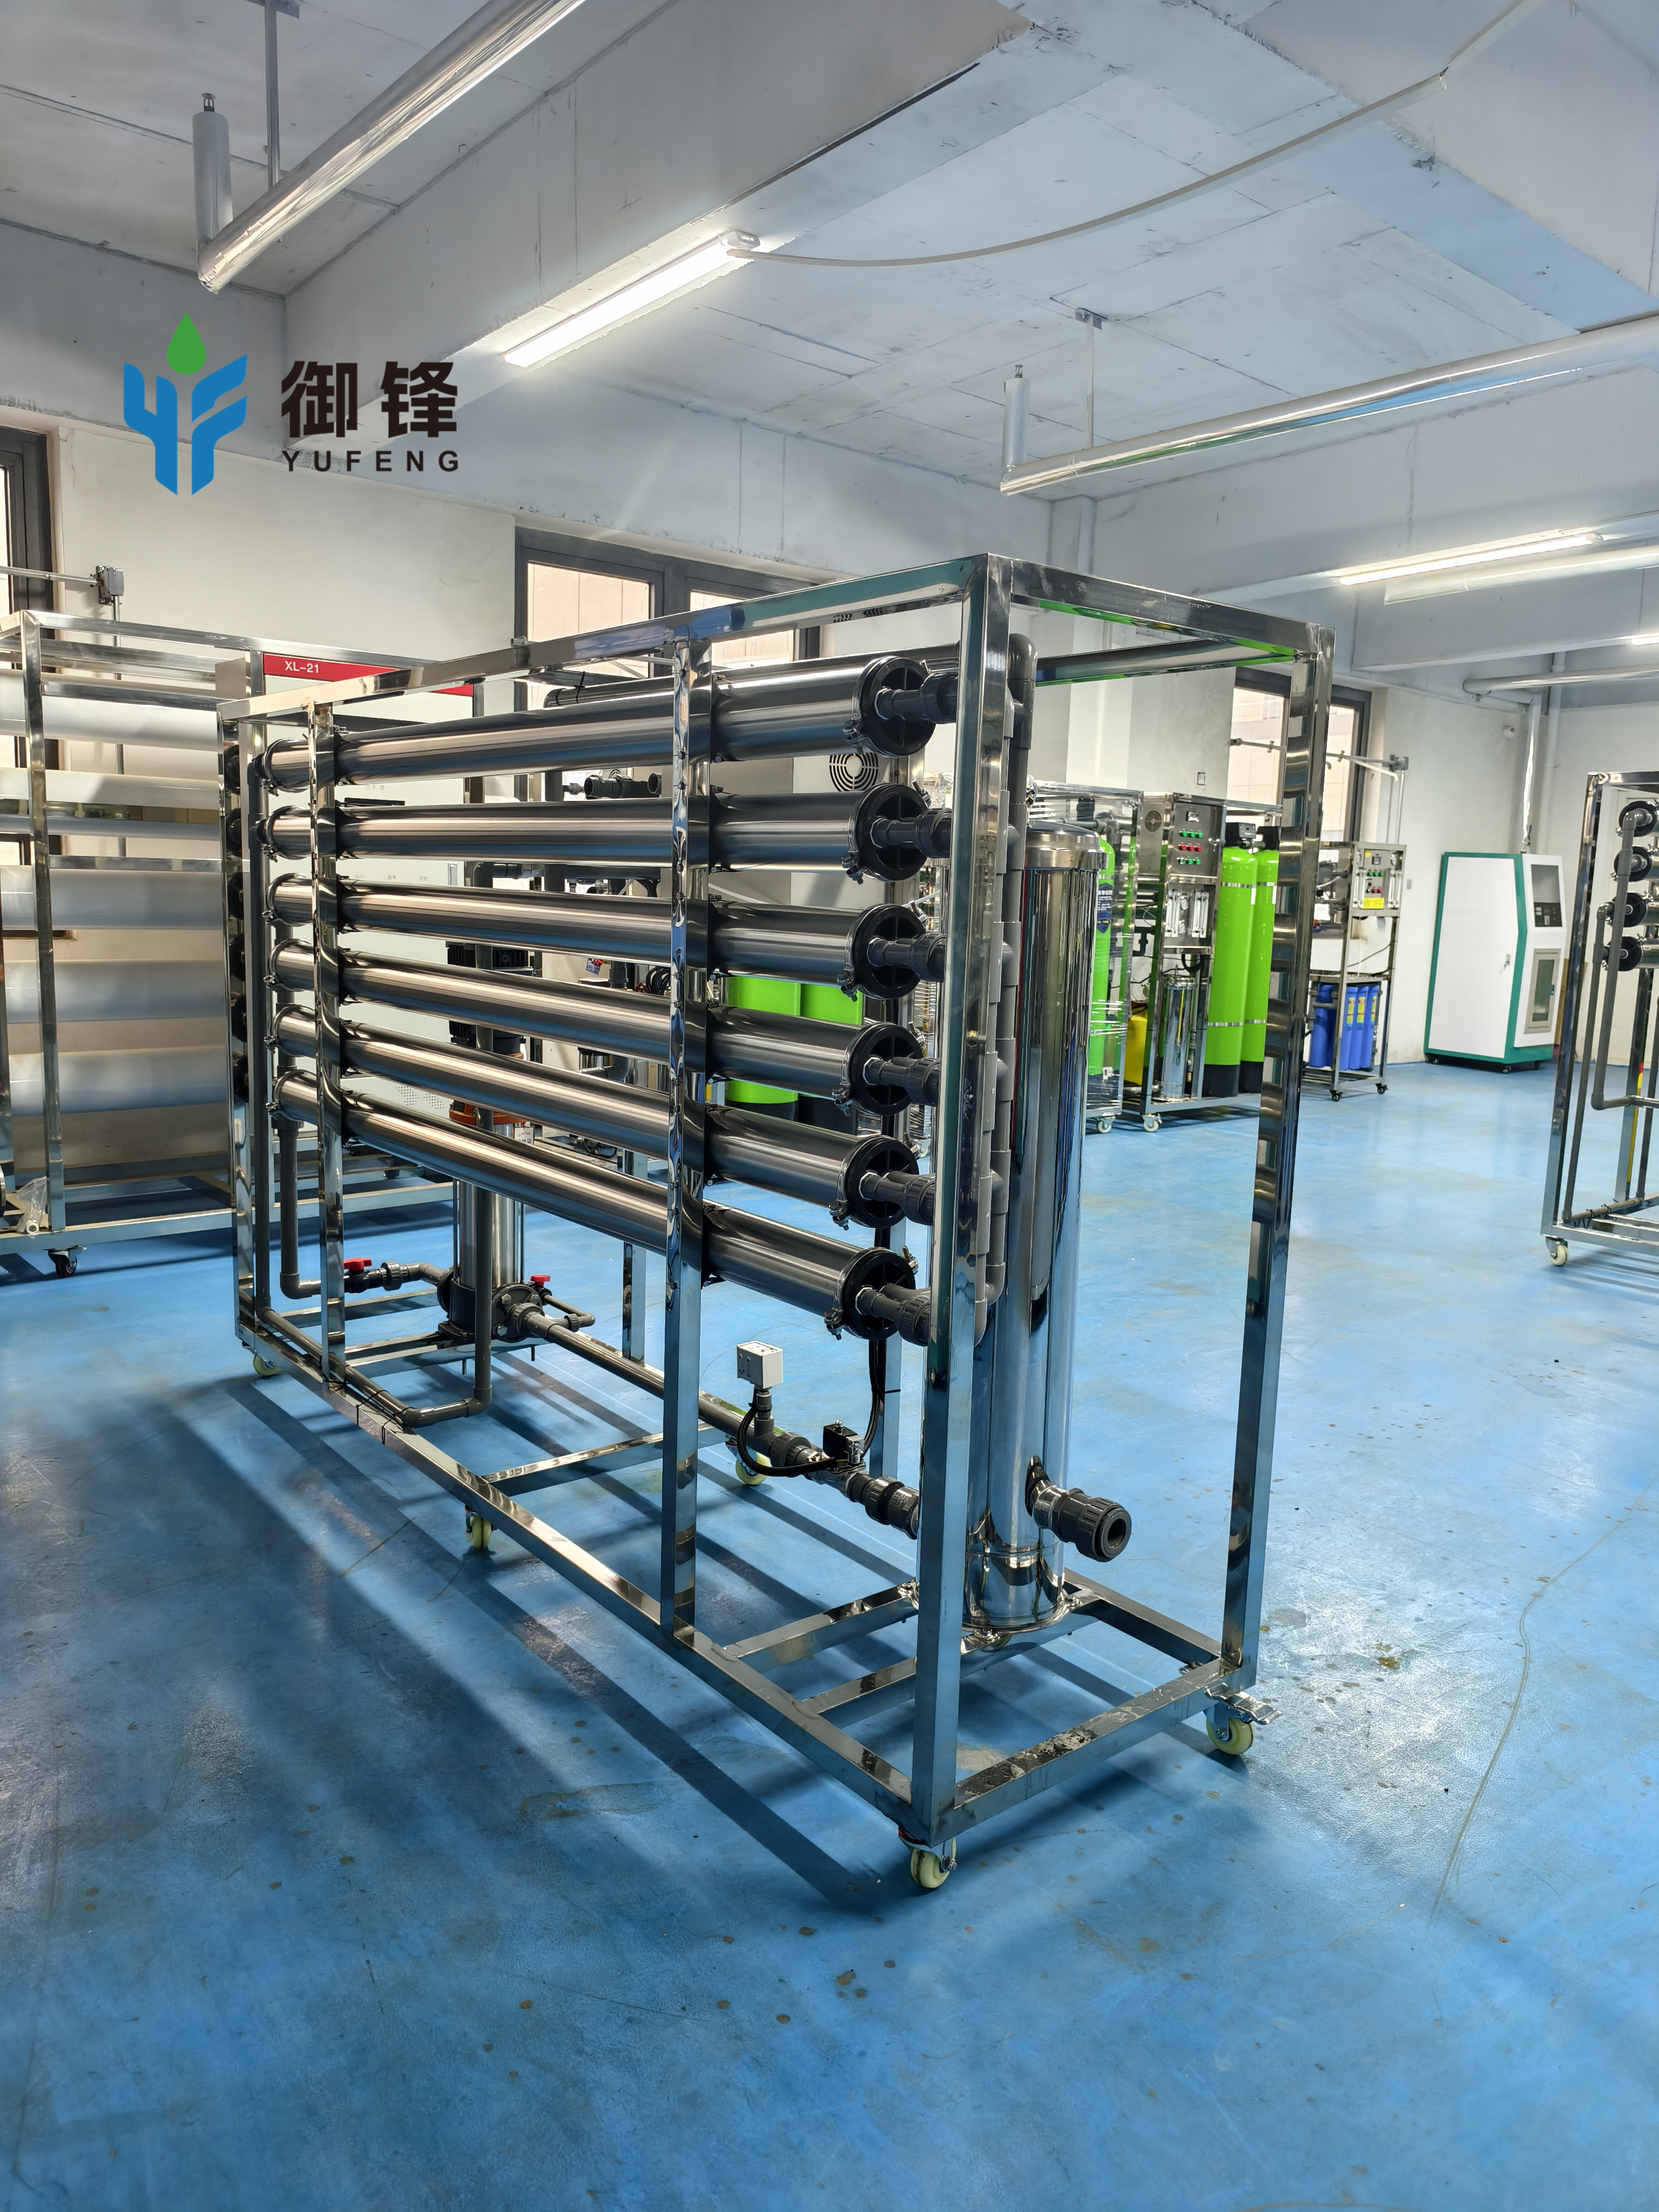
The Industrial Reverse Osmosis Water Purification System is a high-efficiency water treatment solution engineered to remove dissolved salts, impurities, bacteria, viruses, heavy metals, and suspended solids from various water sources. Designed for industrial and commercial applications, the system delivers consistent high-quality purified water while reducing operating costs and maintenance requirements.
Whether treating groundwater, well water, tap water, or surface water, this RO system provides reliable performance and can be customized according to local water conditions and production requirements.
Working Process
Raw Water Tank → Raw Water Pump → Quartz Sand Filter → Activated Carbon Filter → Water Softener (Optional) → Precision Filter → High-Pressure Pump → Reverse Osmosis Membrane System → Pure Water Tank
The multi-stage purification process effectively removes:
Sediment and suspended particles
Chlorine and organic contaminants
Water hardness minerals
Dissolved salts and TDS
Heavy metals
Bacteria and microorganisms
Key Features
✅ High Salt Rejection Rate up to 99%
✅ Stable and Continuous Water Production
✅ Energy-Efficient Design
✅ Fully Automatic PLC Control Available
✅ Premium RO Membranes for Long Service Life
✅ Stainless Steel Frame Optional
✅ Customizable Capacity from 250LPH to 100TPH
✅ Easy Installation and Maintenance
✅ Suitable for Various Water Sources
Technical Advantages
Advanced Reverse Osmosis Technology
Utilizes high-performance RO membranes capable of removing microscopic contaminants and dissolved solids, producing clean and safe water for industrial use.
Intelligent Control System
Optional PLC touchscreen control allows automatic operation, fault monitoring, pressure protection, and real-time performance tracking.
Modular Design
The system can be configured with pretreatment units, softeners, ultrafiltration, EDI modules, UV sterilizers, and ozone generators to meet different water quality requirements.
Durable Construction
Manufactured using high-quality components and corrosion-resistant materials to ensure long-term reliability under demanding operating conditions.
Applications
The Industrial RO Water Purification System is widely used in:
Food & Beverage Industry
Pharmaceutical Manufacturing
Electronics & Semiconductor Production
Chemical Processing
Boiler Feed Water Treatment
Drinking Water Production
Hotels & Resorts
Hospitals & Laboratories
Bottled Water Plants
Industrial Manufacturing Facilities
Why Choose Yufeng Water Treatment?
With over 10 years of experience in water treatment equipment manufacturing, Yufeng provides customized water purification solutions for customers worldwide.
OEM & ODM Support
Professional Engineering Team
Customized System Design
Factory Direct Pricing
Global Installation Guidance
Comprehensive After-Sales Service
FAQ Schema Content
Q1: What water sources can this RO system treat?
The system can treat groundwater, well water, municipal tap water, river water, and other industrial water sources after proper pretreatment.
Q2: What capacities are available?
Standard capacities range from 250LPH to 100TPH, with customized solutions available for larger projects.
Q3: What is the salt removal rate?
The RO membrane system typically achieves 95%-99% salt rejection depending on feed water quality and membrane selection.
Q4: Can the system be customized?
Yes. We can customize capacity, voltage, control system, membrane brand, tank material, and additional treatment stages according to your requirements.
Q5: Do you provide installation support?
Yes. We offer installation guidance, operation training, technical documentation, and after-sales support for overseas customers.

Address: No. 315, Jiefang Road, Lanshan District, Linyi City, Shandong Province, China

+8618553987893
yufengscl@outlook.com
Shandong Yufeng Water Treatment Equipment Co., Ltd

