Professional industrial water treatment equipment manufacturer in China, specializing in RO systems, reverse osmosis equipment, water purification systems, wastewater treatment and customized water treatment solutions for global industries.
Professional industrial water treatment equipment manufacturer in China, specializing in RO systems, reverse osmosis equipment, water purification systems, wastewater treatment and customized water treatment solutions for global industries.

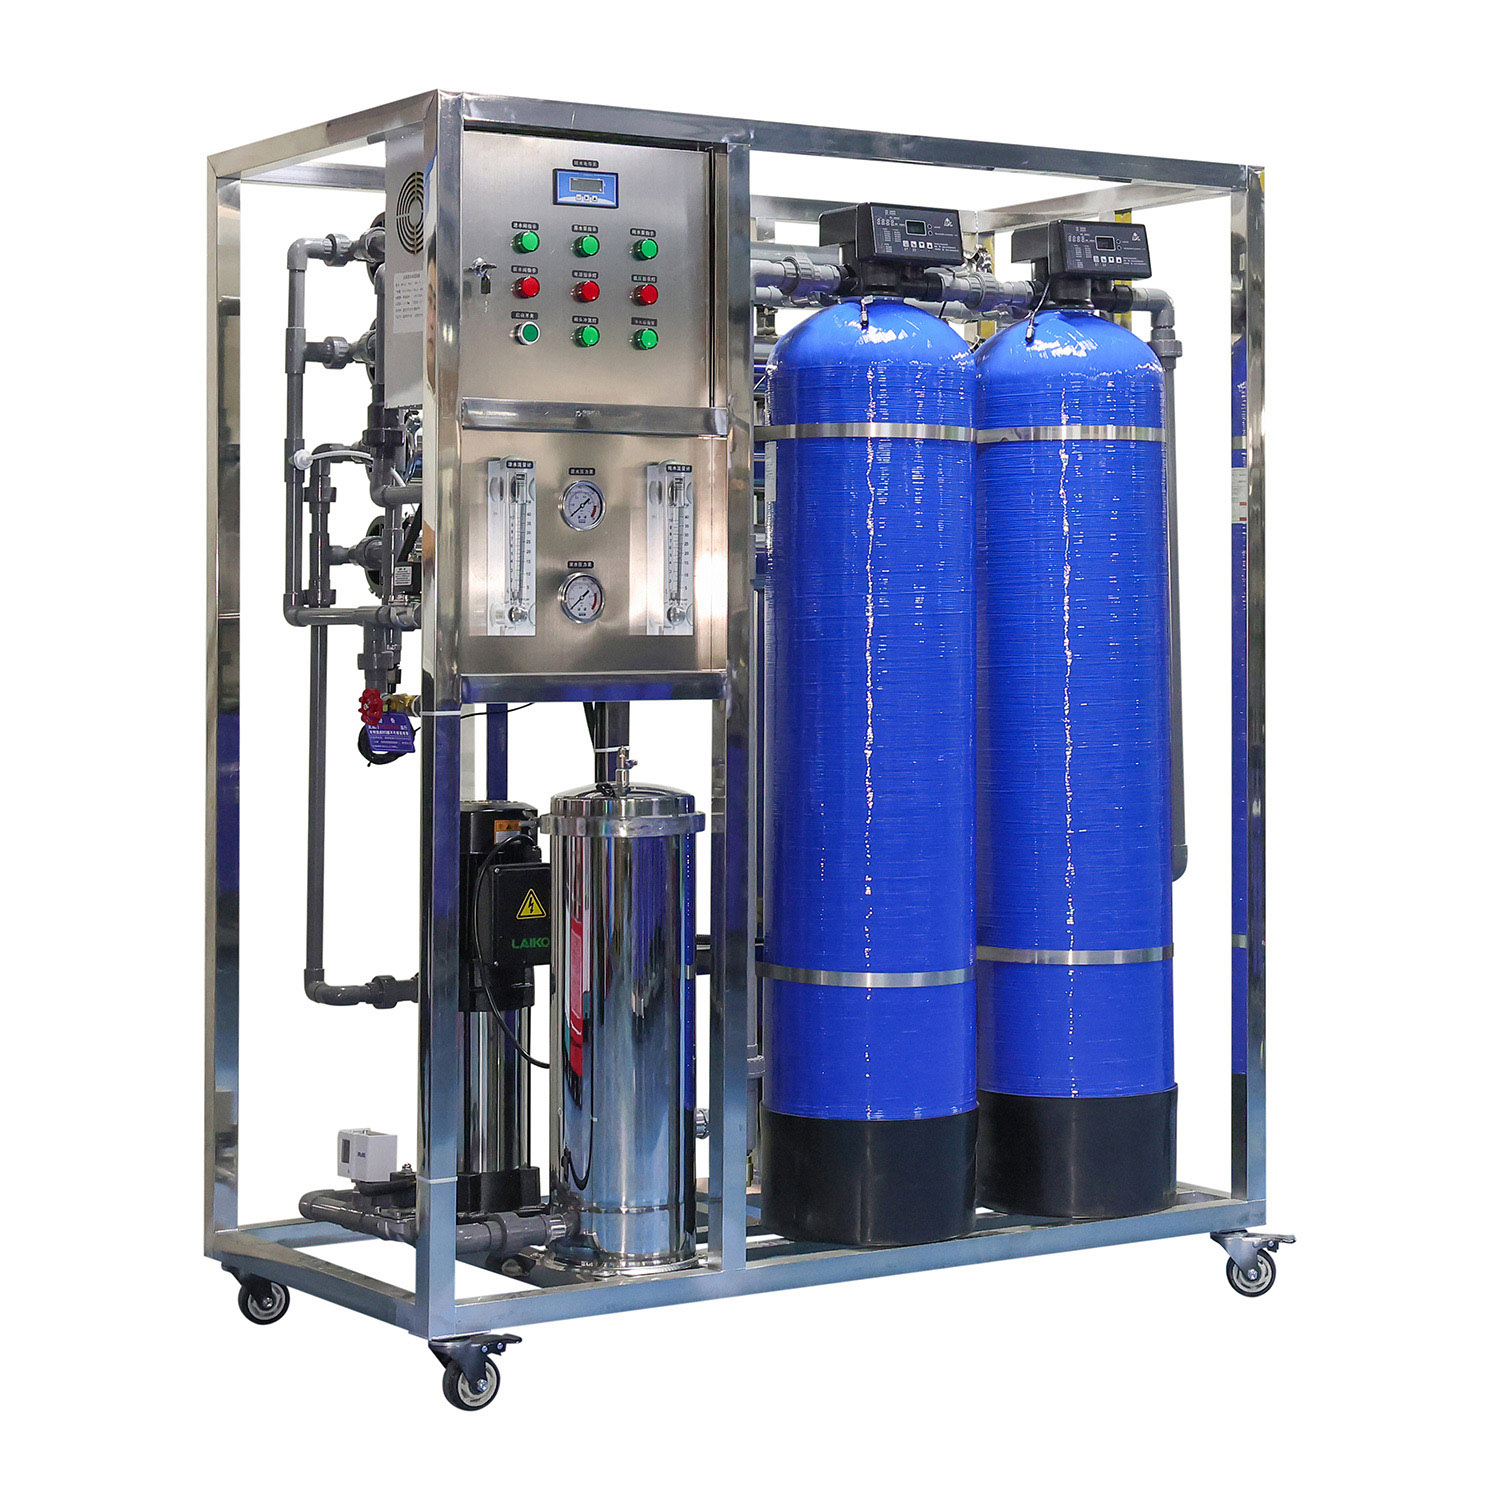
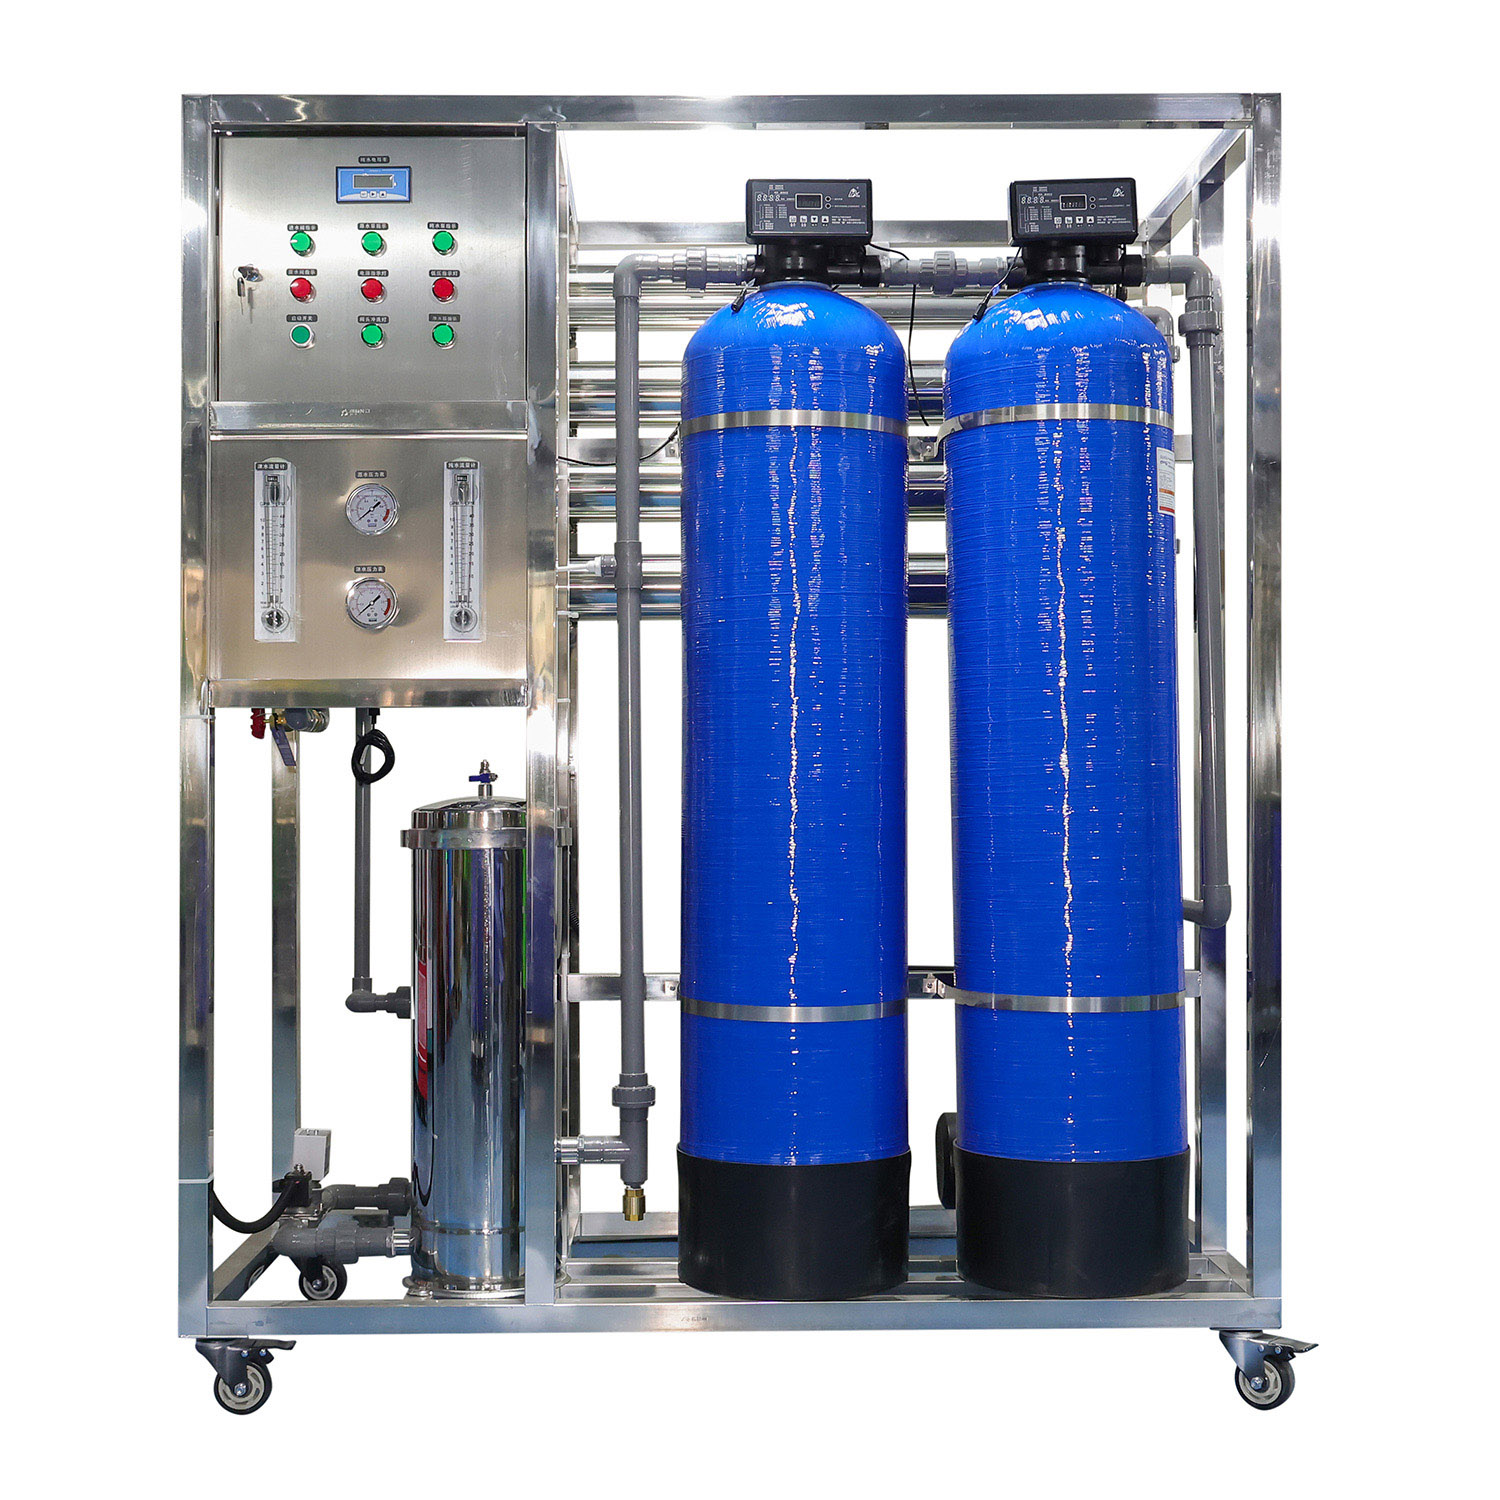
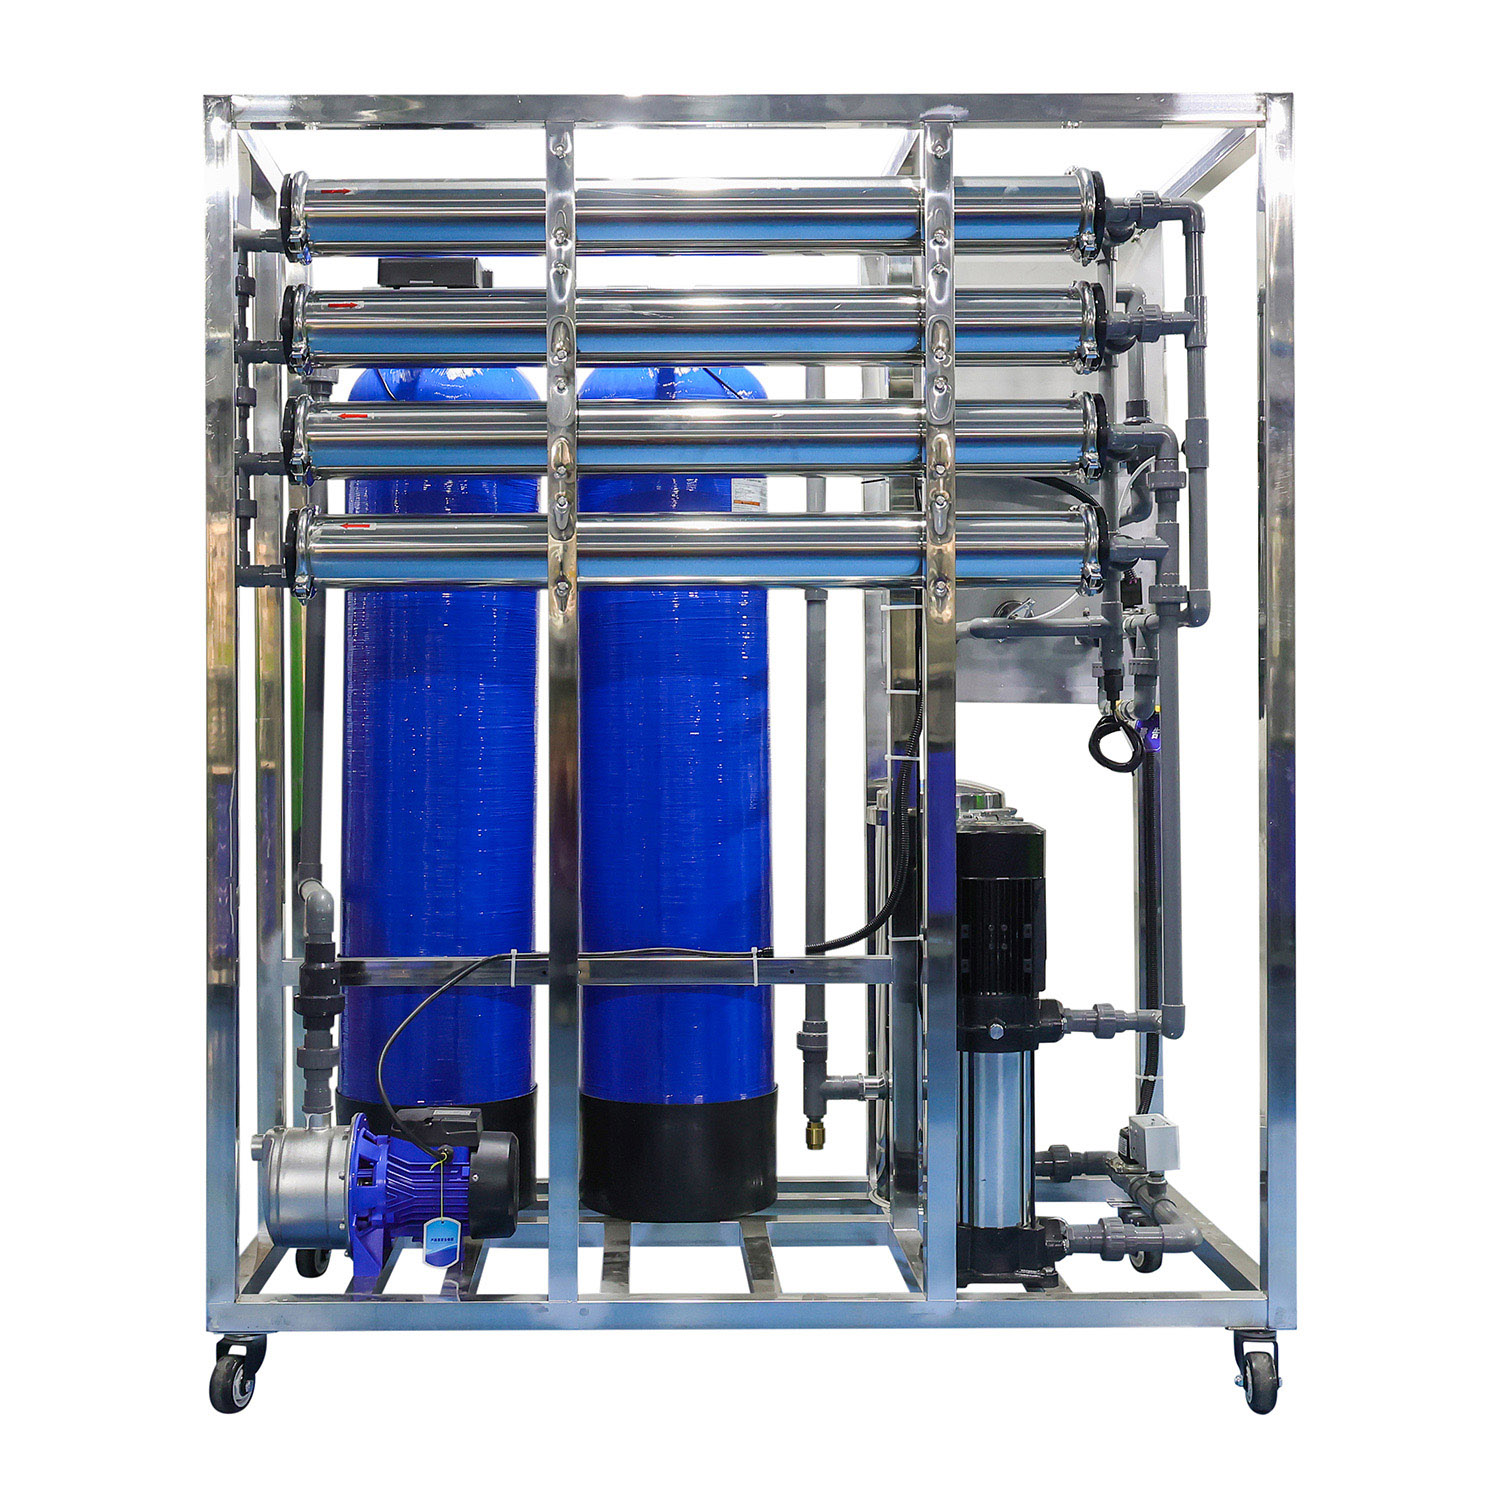
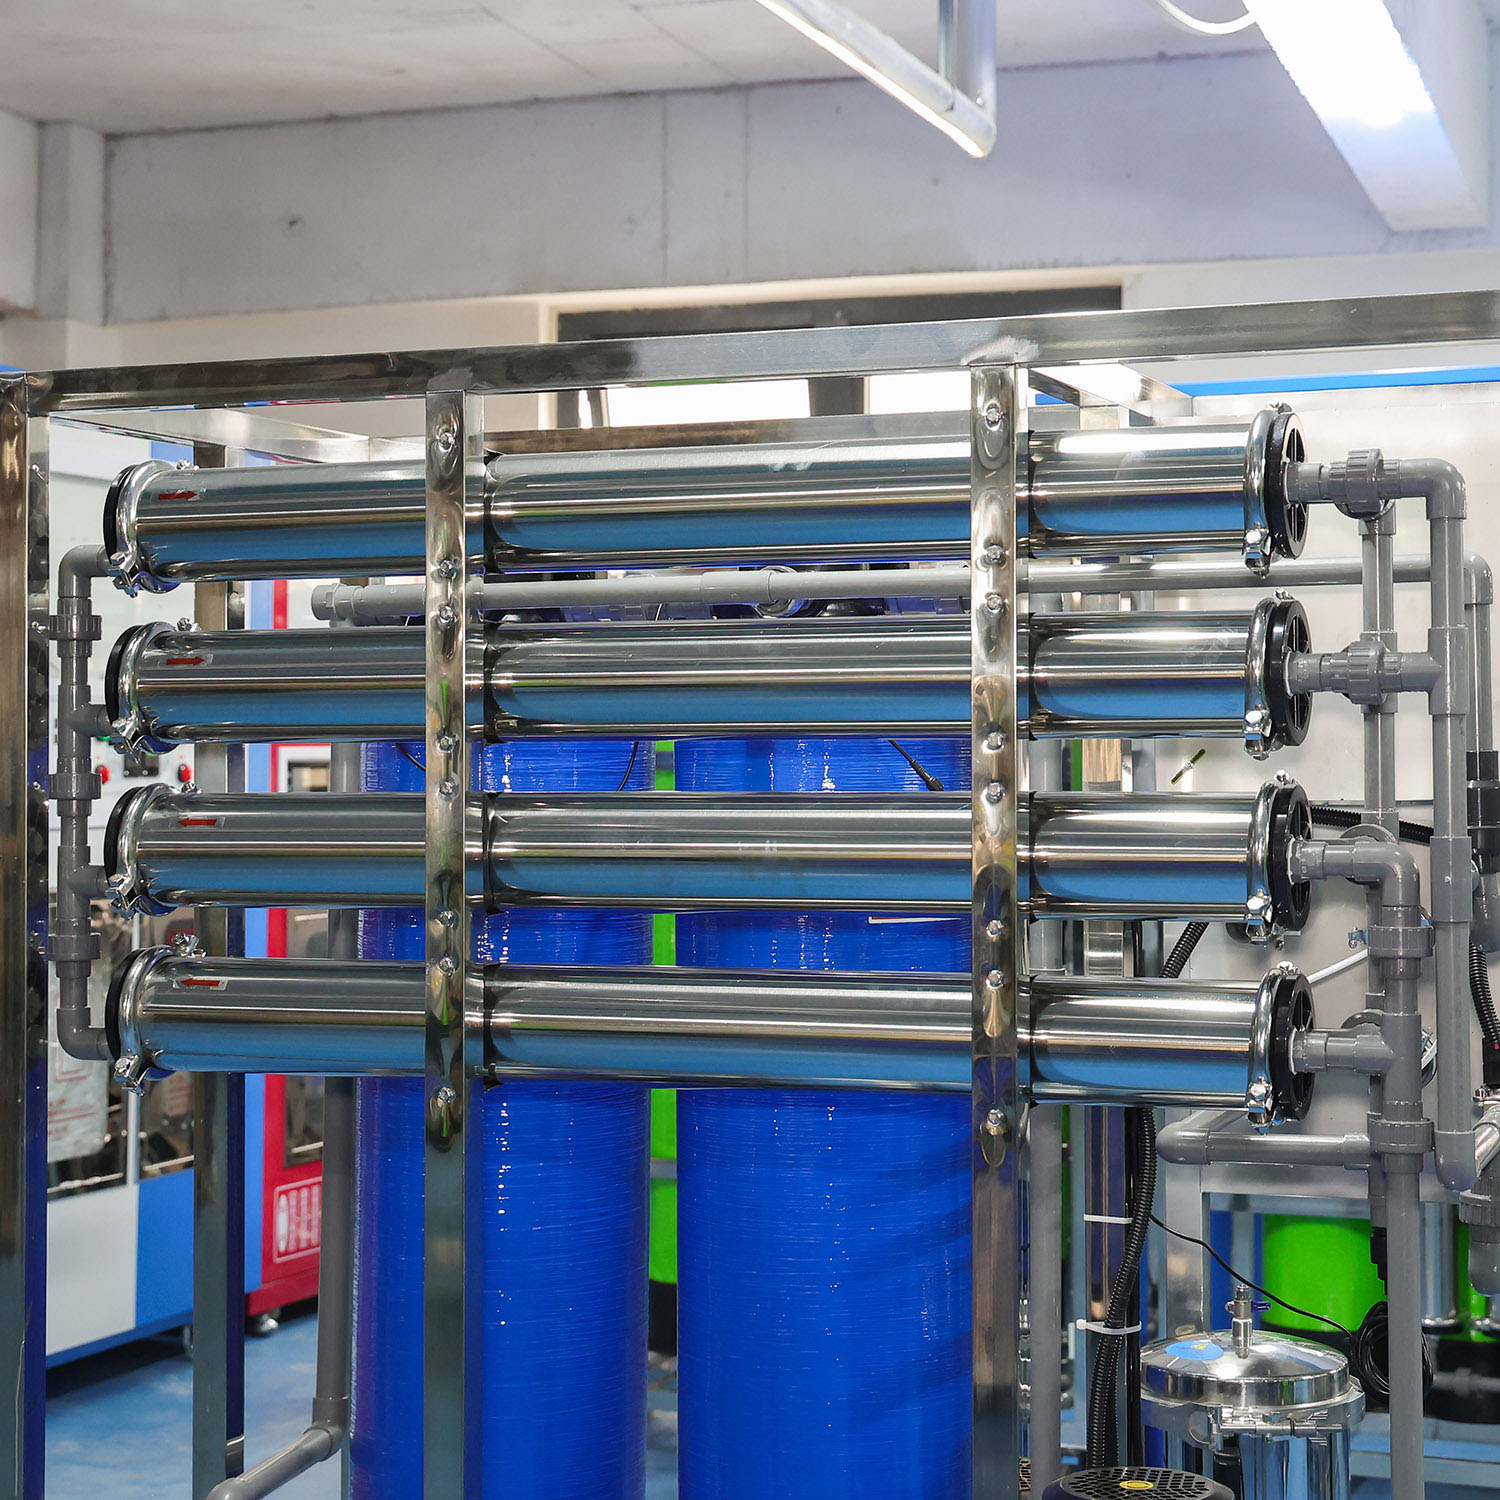


RO Water System 1000LPH | Sand Carbon RO Equipment
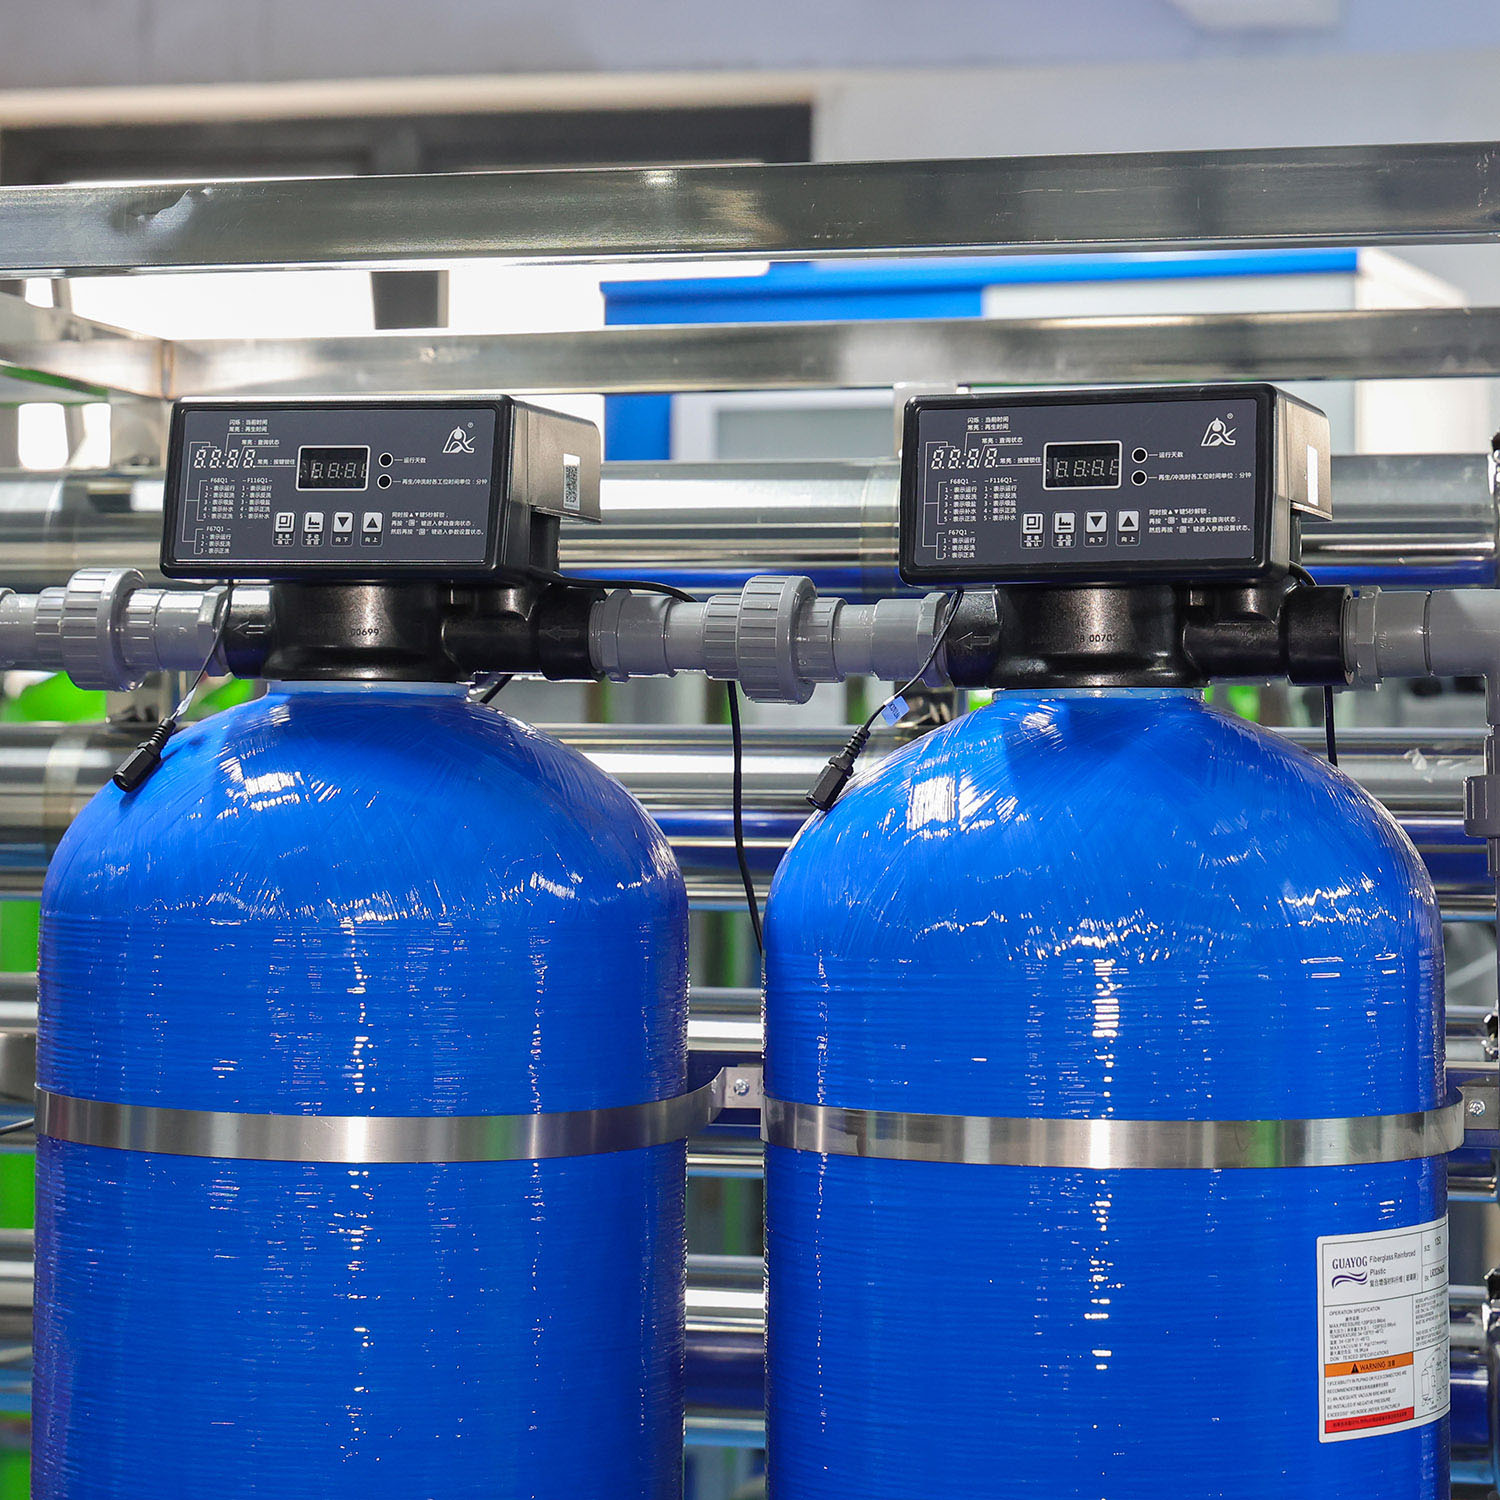
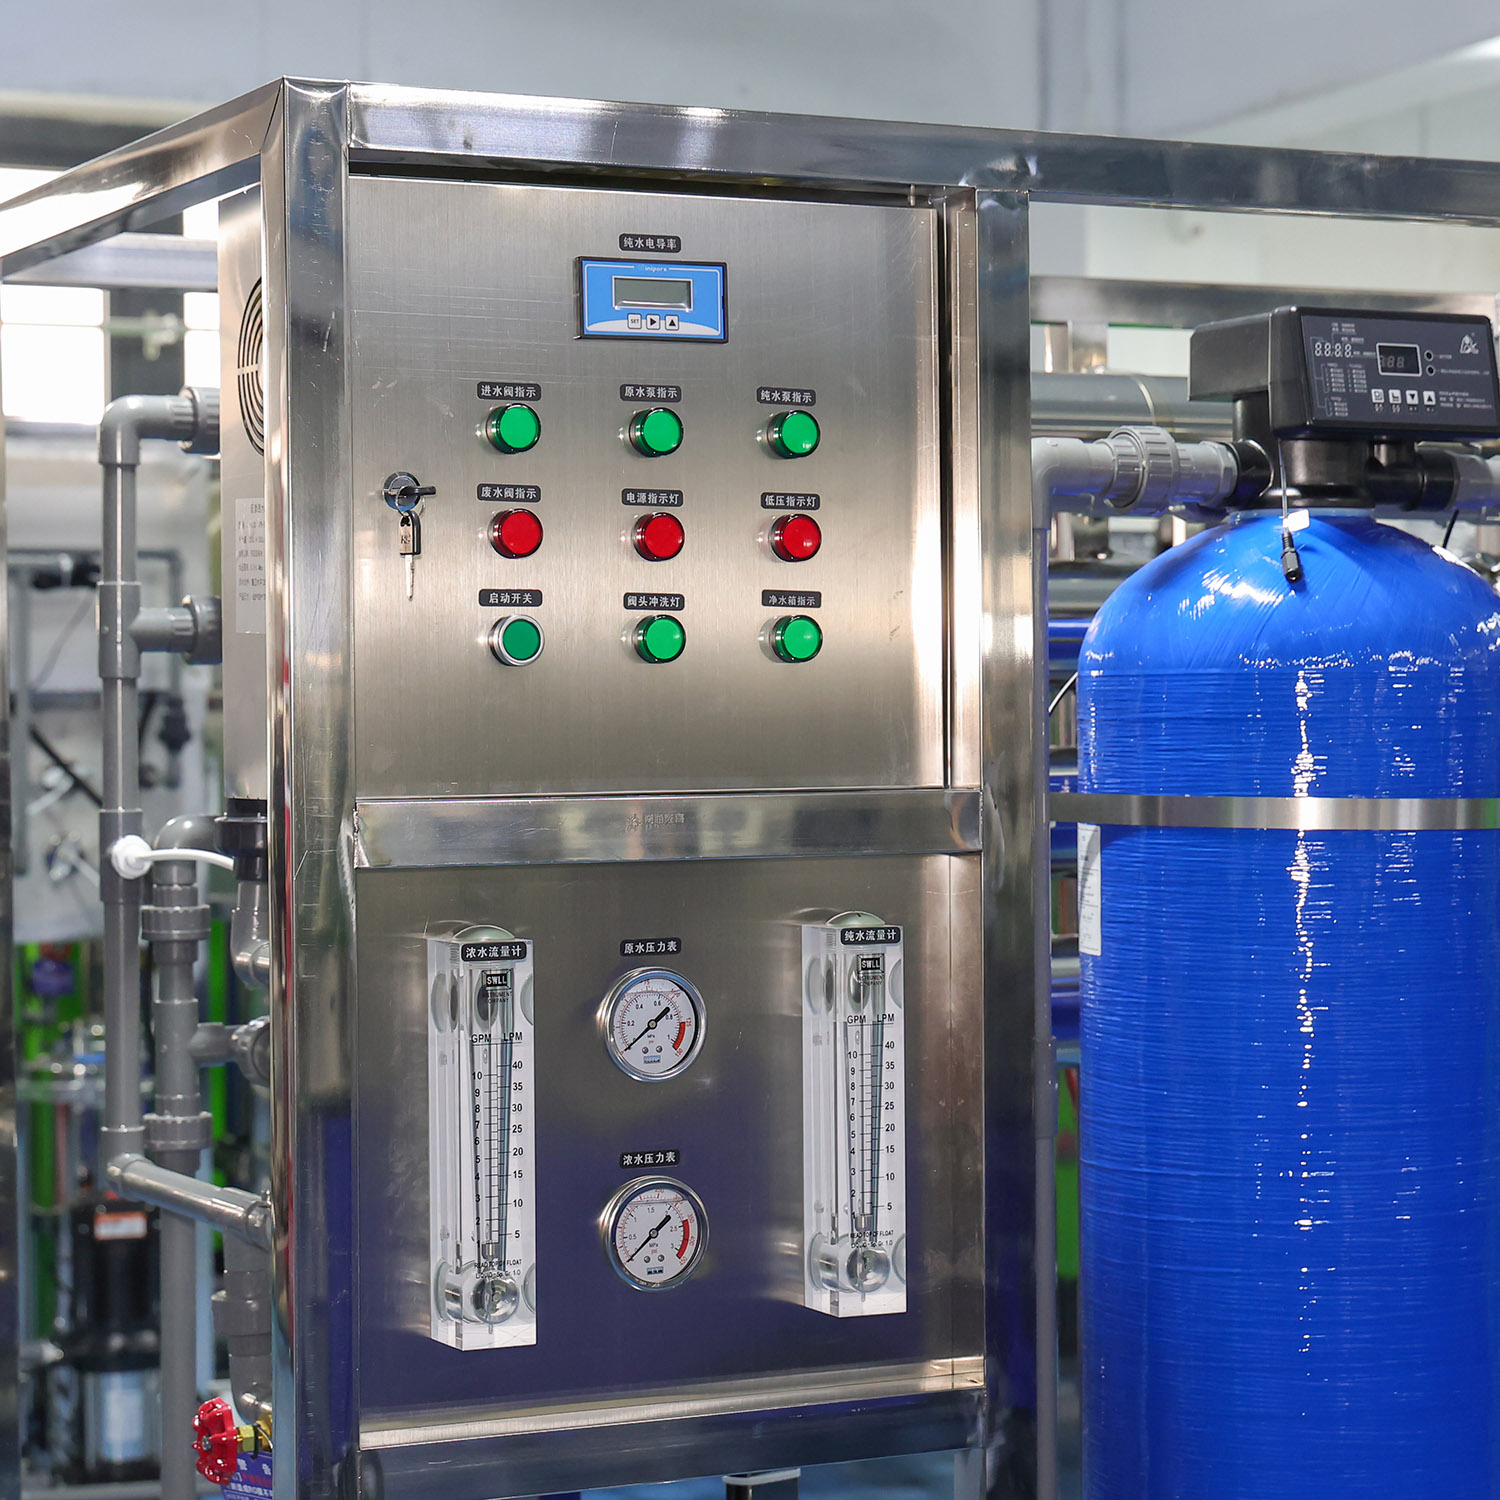
1000LPH RO Water System with Sand and Activated Carbon Filters
Industrial Reverse Osmosis Water Treatment Equipment
Looking for a reliable RO Water System for your factory or commercial water treatment project?
Shandong Yufeng Water Treatment Equipment Co., Ltd. supplies industrial reverse osmosis water treatment equipment designed to reduce dissolved salts and impurities in water. This 1000LPH RO Water System combines sand filtration, activated carbon filtration, precision filtration, and reverse osmosis membrane technology to provide purified water for a variety of industrial and commercial applications.
The system configuration can be selected according to your raw water quality, required water production capacity, and final water quality requirements.
Rated Water Production Capacity: 1,000 Liters Per Hour (1000LPH)
Product Overview
The 1000LPH industrial RO Water System is designed for applications requiring a continuous supply of purified water.
The pretreatment section helps remove suspended particles and reduce residual chlorine before water enters the reverse osmosis unit. The RO membranes then reduce dissolved salts and other impurities, helping improve the quality of the product water.
With a suitable configuration, this system can be used in manufacturing facilities, commercial water treatment projects, food processing plants, and other industrial applications.
How Does the RO Water System Work?
The system uses a multi-stage water treatment process to improve water quality.
Treatment Process:
Raw Water → Sand Filter → Activated Carbon Filter → Precision Filter → High-Pressure Pump → RO Membrane → Purified Water Outlet
1. Sand Filtration
The sand filter helps remove suspended solids, sediment, and particulate matter from the feed water. This pretreatment stage helps reduce the filtration load on downstream equipment.
2. Activated Carbon Filtration
The activated carbon filter helps reduce residual chlorine and certain organic compounds. Proper chlorine removal is important for protecting chlorine-sensitive reverse osmosis membranes.
3. Precision Filtration
The precision filter captures additional particles before water enters the RO membrane assembly, helping protect the membrane system.
4. Reverse Osmosis Purification
The high-pressure pump supplies the pressure required for reverse osmosis. The RO membranes separate a portion of dissolved salts and other impurities from the feed water to produce purified water.
Actual water quality and production capacity depend on feed water conditions, operating pressure, temperature, membrane selection, and system design.
Key Features of Our 1000LPH RO Water System
Rated Capacity of 1000LPH
Designed for a rated purified water output of 1,000 liters per hour under specified operating conditions.
Integrated Sand and Carbon Pretreatment
Combines sand filtration and activated carbon filtration to help protect the RO membranes and improve pretreatment performance.
Reverse Osmosis Membrane Technology
Reduces dissolved salts and many impurities, with final water quality determined by the source water and system configuration.
Continuous Water Supply
Designed for continuous operation when the system is correctly configured, installed, and maintained.
Flexible Equipment Configuration
Membrane selection, pumps, electrical components, control systems, and other specifications can be discussed according to project requirements.
Factory Direct Supply
Shandong Yufeng Water Treatment Equipment Co., Ltd. provides water treatment equipment solutions for overseas distributors, engineering contractors, and industrial end users.
Technical Specifications
Product Name: 1000LPH RO Water System
Product Type: Industrial Reverse Osmosis Water Treatment Equipment
Rated Water Production Capacity: 1,000 LPH (1 Ton/Hour)
Pretreatment System: Sand Filter + Activated Carbon Filter
Fine Filtration: Precision Filter
Main Purification Technology: Reverse Osmosis (RO)
Feed Water Source: To be confirmed according to actual equipment configuration
RO Membrane Brand and Quantity: To be confirmed
Pump Specifications: To be confirmed
Control System: To be confirmed
Power Supply: Configurable according to destination country and project requirements
Customization: Available upon confirmation
Note: Final technical specifications should be confirmed according to the selected equipment configuration and raw water conditions.
Applications of the RO Water System
Industrial Manufacturing
Provides purified process water for suitable industrial production applications.
Food and Beverage Processing
Can be configured for food processing water applications, subject to applicable hygiene requirements and the required water quality standards.
Boiler Feedwater Pretreatment
Can serve as a reverse osmosis treatment stage for boiler makeup water systems. Additional treatment may be necessary depending on boiler pressure and water quality requirements.
Commercial Water Treatment
Suitable for commercial water purification projects requiring a rated capacity of approximately 1,000 liters per hour.
Water Treatment Engineering Projects
Can be incorporated into customized water treatment systems based on the project's source water and target water quality.
Why Choose Shandong Yufeng Water Treatment Equipment Co., Ltd.?
Shandong Yufeng Water Treatment Equipment Co., Ltd. specializes in water treatment equipment solutions, including reverse osmosis systems, ultrafiltration equipment, water softeners, and industrial water purification systems.
We work with distributors, engineering contractors, and industrial customers to discuss equipment configurations based on application requirements.
Our team can help evaluate the required production capacity, raw water conditions, target water quality, and local electrical specifications before confirming a suitable system.
Request a Quote for Your RO Water System
Looking for a 1000LPH RO Water System for your business?
Contact us with the following information:
Raw water source: tap water, groundwater, or another source
Required water production capacity
Target water quality or conductivity
Application of the purified water
Destination country and local power supply
Our team can review your requirements and recommend a suitable configuration for your project.
Contact Shandong Yufeng Water Treatment Equipment Co., Ltd. today to discuss your industrial RO water treatment requirements.


Address: No. 315, Jiefang Road, Lanshan District, Linyi City, Shandong Province, China

+8618553987893
yufengscl@outlook.com
Shandong Yufeng Water Treatment Equipment Co., Ltd

